Intelligent material pneumatic conveying has become a critical technology in modern industrial processes, especially for handling bulk materials in various sectors. This article delves into the fundamental aspects of this technology, focusing on its design principles and practical applications.
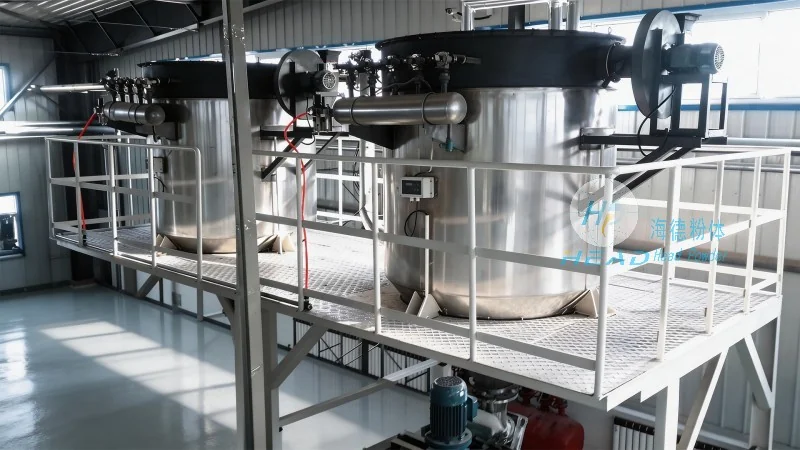
Introduction to Intelligent Material Pneumatic Conveying
Intelligent material pneumatic conveying refers to the automated and efficient transport of bulk materials using air or other gases as the conveying medium. Unlike traditional methods that rely on mechanical components like belts or buckets, this system leverages pneumatic pressure to move materials through pipelines. The "intelligent" aspect of the system often involves advanced control systems, sensors, and data analytics to optimize performance, ensure safety, and enhance operational efficiency.
Core Concept of Material Pneumatic Conveying
At its core, material pneumatic conveying works by creating a pressure differential between the inlet and outlet of the conveying line. The system typically consists of a blower or compressor that generates the necessary air flow, a hopper or feeder to introduce the material, and a receiver or discharge point where the material is collected. The air and material mixture travels through the pipeline, with the air providing the force to move the material. This method is particularly effective for materials that are difficult to handle mechanically, such as powders, granules, and fine particles.
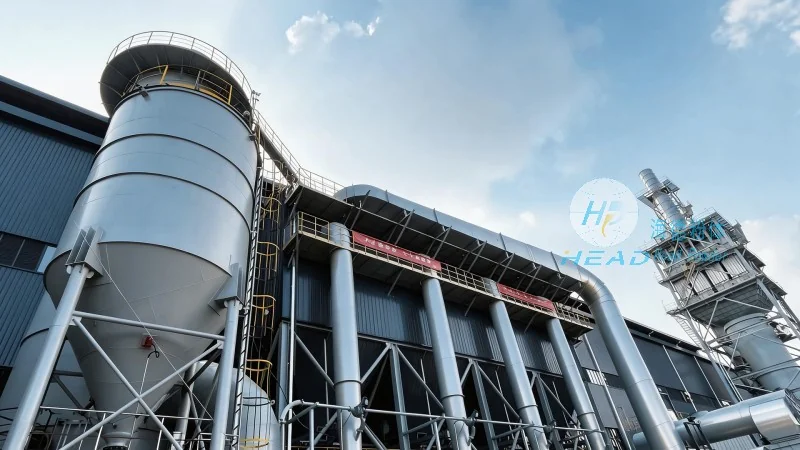
Design Principles of Intelligent Material Pneumatic Conveying Systems
The design of intelligent material pneumatic conveying systems follows several key principles to ensure reliability, efficiency, and safety. First, the system must be tailored to the specific characteristics of the material being conveyed, including its density, flowability, and moisture content. This involves selecting the appropriate type of conveying system—such as dilute-phase or dense-phase—and determining the optimal air velocity and pressure. Second, the system incorporates advanced control mechanisms to monitor and adjust parameters in real-time. Sensors are used to detect material levels, air pressure, and flow rates, while data analytics help identify potential issues and optimize performance. Third, the design emphasizes safety features, such as explosion-proof components for hazardous materials and emergency shut-off systems to prevent accidents. Finally, the system is built for scalability and adaptability, allowing it to be integrated into existing production lines or expanded as production needs grow.
Key Components and Their Functions
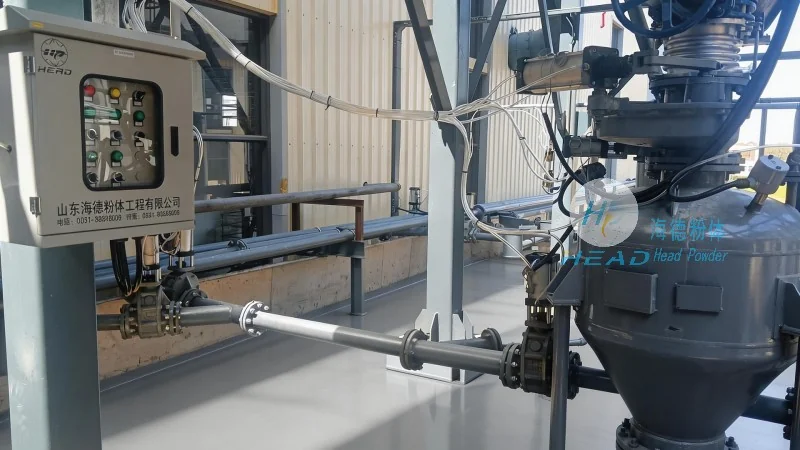
Several key components make up an intelligent material pneumatic conveying system. The blower or compressor is the primary source of air pressure, providing the force to move the material. The hopper or feeder is responsible for feeding the material into the system, ensuring a consistent flow. The pipeline network connects the various components and transports the material from the inlet to the outlet. The receiver or discharge point collects the material and may include a filter or separator to remove excess air. Additionally, the system may include a control panel with sensors and a programmable logic controller (PLC) to manage the operation and monitor performance. These components work together to create a seamless and efficient material transport process.
Application Scenarios and Benefits
Intelligent material pneumatic conveying is widely used in various industries, including pharmaceuticals, food processing, chemicals, and manufacturing. In the pharmaceutical industry, for example, it is used to transport raw materials and finished products with high precision and minimal contamination. In food processing, it ensures hygienic handling of ingredients, preventing cross-contamination and maintaining product quality. The benefits of this technology include improved safety, reduced labor costs, increased production efficiency, and lower maintenance requirements compared to traditional methods. Additionally, the intelligent features allow for real-time monitoring and data-driven decision-making, further enhancing operational performance.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of intelligent material handling solutions. With a strong focus on innovation and quality, the company specializes in designing and manufacturing pneumatic conveying systems tailored to the needs of various industries. HeadPowder's products are known for their reliability, efficiency, and advanced features, making them a trusted choice for businesses seeking to optimize their material handling processes. The company is committed to providing comprehensive support, from system design and installation to maintenance and after-sales service, ensuring that clients achieve maximum value from their investment. HeadPowder is headquartered in Shandong, China, and serves customers worldwide with its expertise and dedication to excellence.




