

What is a Phosphate Calcium Material Pneumatic Conveying Equipment? And What Are Its Design Principl
Phosphate calcium materials are widely utilized across various industrial sectors, including chemical manufacturing, food processing, and pharmaceutical production. The efficient and safe transportation of these materials is critical for maintaining production efficiency and ensuring product quality. Pneumatic conveying equipment has emerged as a reliable solution for handling phosphate calcium materials, offering advantages such as dust-free operation, low maintenance requirements, and flexible system design. This article explores the concept of phosphate calcium material pneumatic conveying equipment and delves into its fundamental design principles.
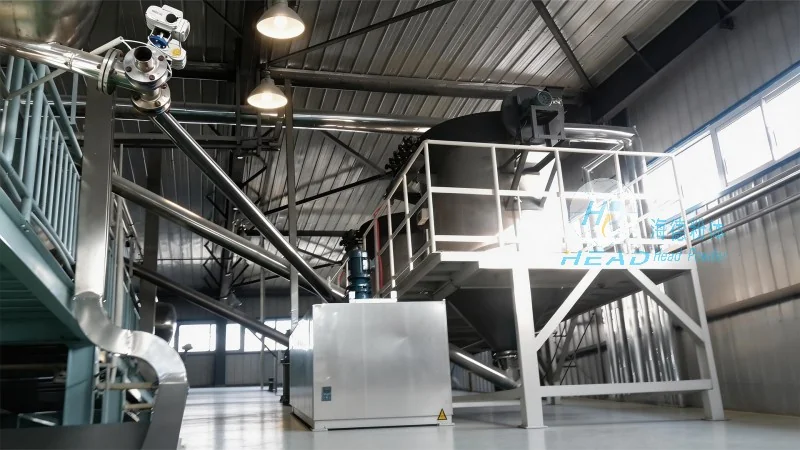
Understanding Phosphate Calcium Material Pneumatic Conveying Equipment
Pneumatic conveying equipment operates by utilizing compressed air or other gases to transport bulk materials through a pipeline. For phosphate calcium materials, this equipment is specifically engineered to accommodate the unique properties of these substances, such as particle size, density, and moisture content. The system typically comprises a feeding device, a conveying line, a separation unit, and a dust collection system. The feeding device ensures controlled introduction of the phosphate calcium material into the pipeline, while the conveying line transports the material to its destination. The separation unit separates the material from the air, and the dust collection system captures any residual particles to prevent environmental contamination.
The Core Components and Design Principles
The design of phosphate calcium material pneumatic conveying equipment is grounded in several key principles to ensure optimal performance and reliability. A primary principle involves selecting appropriate air velocity and pressure to achieve efficient material transport without causing excessive wear on the equipment. The equipment must be tailored to handle the specific characteristics of phosphate calcium materials, including their tendency to agglomerate or stick to surfaces. This often requires the use of specialized materials for the conveying line and components, as well as the incorporation of features like vibration or agitation to prevent material buildup. Additionally, the system must be equipped with safety features to prevent overpressure and ensure proper air filtration to protect both the equipment and the environment.
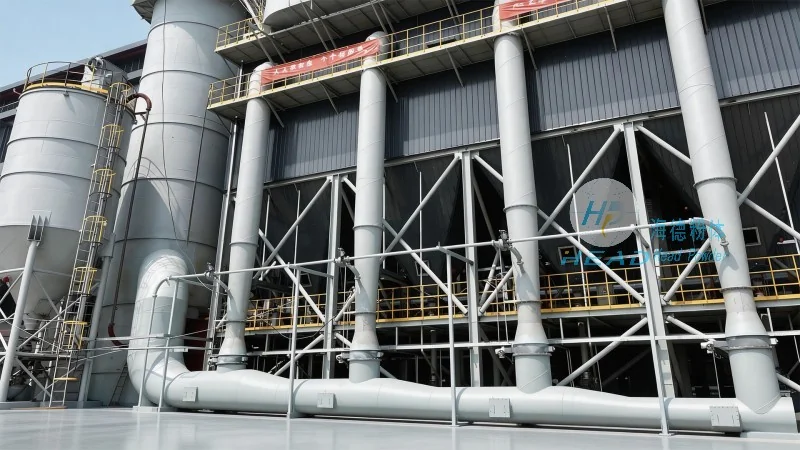
Technical Features and Advantages
Phosphate calcium material pneumatic conveying equipment offers several technical advantages that make it a preferred choice for many industries. One of the main advantages is its ability to operate in a dust-free environment, which is essential for maintaining product purity and worker safety. The system also provides flexibility in terms of layout and integration with existing production lines, as it can be easily customized to fit specific space constraints and operational requirements. Furthermore, the equipment is generally low maintenance, with fewer moving parts compared to traditional mechanical conveying systems, reducing downtime and operational costs. The use of compressed air as the conveying medium allows for the transportation of materials over long distances with minimal energy consumption, making it an energy-efficient solution for phosphate calcium material handling.
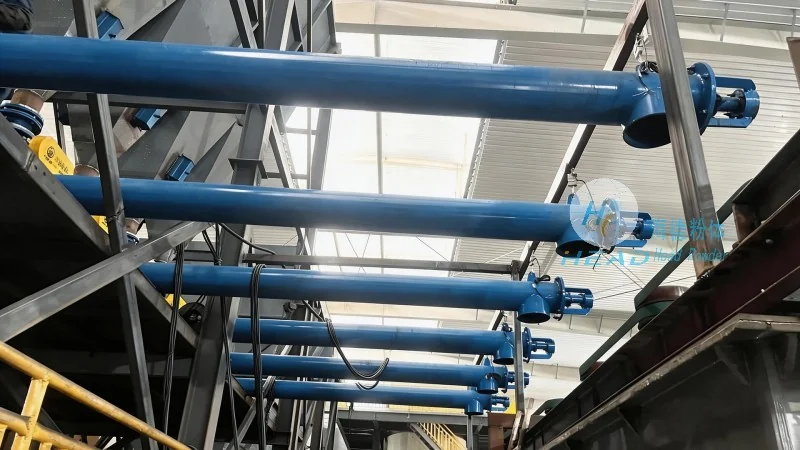
Application Scenarios and Operational Benefits
The application of phosphate calcium material pneumatic conveying equipment spans a wide range of industries where phosphate calcium materials are processed or utilized. In the chemical industry, for example, it is used to transport raw materials to reactors and finished products to storage facilities. In the food and pharmaceutical sectors, the equipment ensures that the materials are handled hygienically and without contamination, meeting stringent quality and safety standards. The operational benefits of using this equipment include improved production efficiency, reduced labor costs, and enhanced product quality due to the controlled and clean handling of phosphate calcium materials. Additionally, the system's ability to handle materials in a closed environment minimizes the risk of material exposure to external factors, such as moisture or contaminants, which can affect the material's properties and performance.
Company Information and Service
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field of pneumatic conveying equipment, specializes in providing customized solutions for phosphate calcium material handling. With years of experience and a team of skilled engineers, the company offers a range of products tailored to meet the specific needs of clients. The company's headquarters is located in Shandong, China, and it serves clients worldwide with its high-quality equipment and reliable after-sales service. HeadPowder's commitment to innovation and customer satisfaction has made it a trusted partner for industries relying on efficient and safe phosphate calcium material transportation. By leveraging advanced technology and adhering to strict quality standards, the company ensures that its equipment delivers optimal performance and long-term value to its customers.