The fly ash silo powder conveying machine is a specialized equipment designed for the efficient handling and transportation of fly ash, a byproduct from coal-fired power plants. This equipment plays a crucial role in modern industrial applications, ensuring the safe and reliable movement of fly ash from storage silos to processing or disposal sites. Understanding its operational principles and the specific working scenarios where it excels is essential for optimizing industrial processes and enhancing operational efficiency.
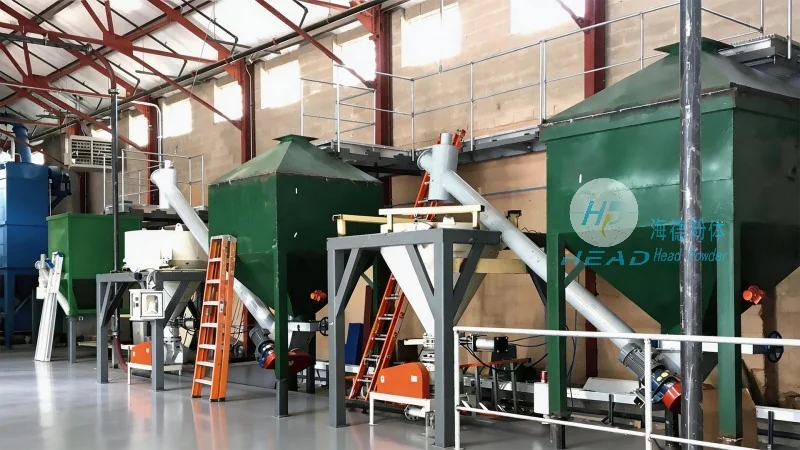
HeadPowder, a leading manufacturer in the field, offers advanced solutions tailored to meet the diverse needs of industrial clients. With a focus on innovation and reliability, the company has developed a range of conveying systems that integrate seamlessly into existing infrastructure. The fly ash silo powder conveying machine from HeadPowder is engineered to handle the unique challenges associated with fly ash, such as its fine particle size, abrasive nature, and potential for dust generation.
The core principle of the fly ash silo powder conveying machine involves the use of positive pressure or vacuum systems to transport the material. Positive pressure systems utilize air blowers to force air and fly ash through a pipeline, while vacuum systems create a negative pressure environment to draw the material. Both methods are designed to maintain the integrity of the fly ash, preventing caking or agglomeration during transport. The machine typically consists of a hopper, a conveyor line, and a control system that monitors and adjusts the flow rate based on real-time conditions.
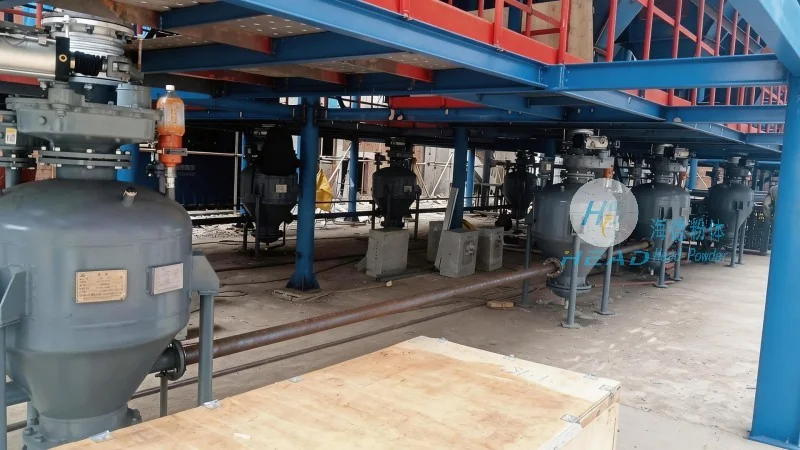
In terms of working scene characteristics, the fly ash silo powder conveying machine is particularly effective in large-scale power plants and industrial facilities where fly ash needs to be moved over significant distances or to different processing units. Its compact design allows for installation in confined spaces, making it suitable for retrofitting into existing plants without major structural modifications. The equipment is also designed to minimize environmental impact by reducing dust emissions through advanced sealing and filtration systems.
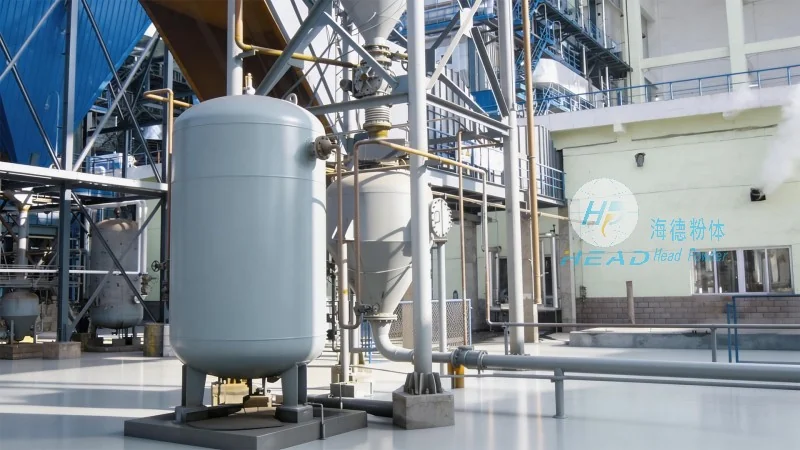
The operational efficiency of the fly ash silo powder conveying machine is enhanced by its automated control features. Sensors and control panels monitor parameters like pressure, flow rate, and temperature, ensuring consistent performance and preventing equipment damage. This automation not only improves safety but also reduces the need for manual intervention, leading to lower labor costs and increased productivity. HeadPowder's machines are equipped with user-friendly interfaces that allow operators to adjust settings quickly and respond to changing operational demands.
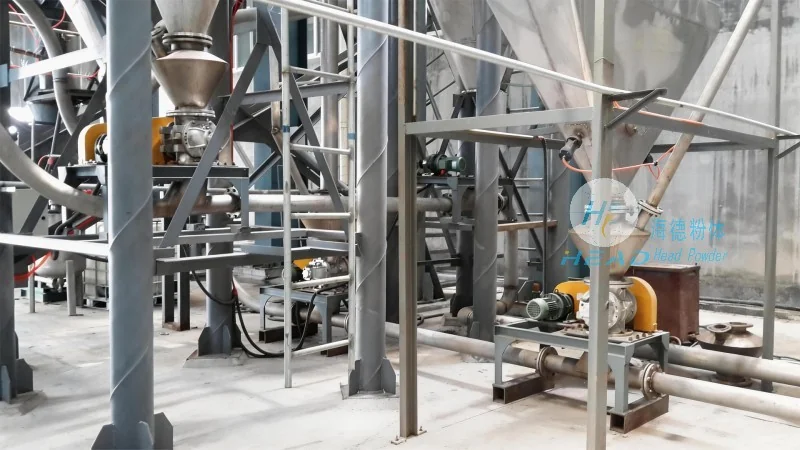
The working scene characteristics also include the ability to handle varying fly ash compositions and moisture levels. The conveying system is designed to accommodate different particle sizes and densities, ensuring that the material is transported without blockages or inefficiencies. This adaptability makes the machine suitable for a wide range of applications, from primary storage to secondary processing, where the fly ash may be used as a raw material in cement production or other industrial processes.
In conclusion, the fly ash silo powder conveying machine from HeadPowder is a reliable and efficient solution for managing fly ash in industrial settings. By understanding its operational principles and the specific working scenarios where it excels, industrial clients can optimize their processes, reduce operational costs, and enhance overall productivity. HeadPowder's commitment to quality and innovation ensures that their equipment meets the highest standards of performance and safety, making it a trusted choice for businesses in the power and industrial sectors.




