HeadPowder, a leading engineering firm based in Shandong, China, specializes in the design and implementation of pneumatic conveying systems tailored for bulk material handling, including barley. This article explores the fundamental principles of pneumatic conveying technology and highlights key application scenarios where such systems excel in transporting barley efficiently and reliably.
Understanding Pneumatic Conveying Principles
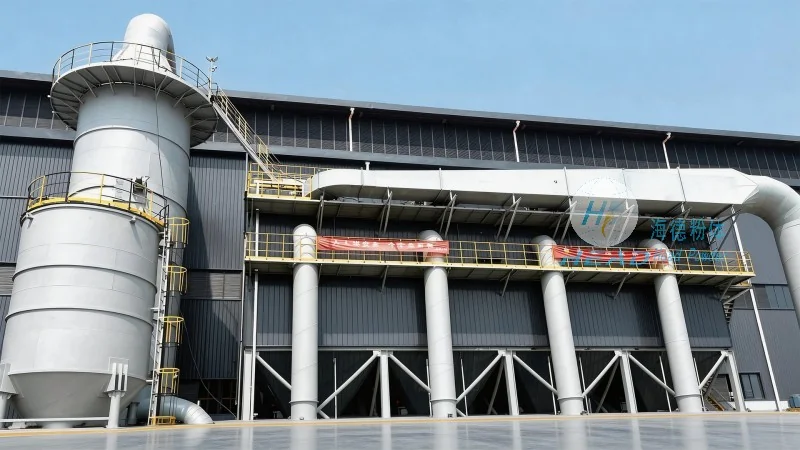
Pneumatic conveying, also known as bulk material handling via air, is a method that uses pressurized or suction air to transport granular or powder materials like barley through a pipeline. The core principle involves creating a flow of air that lifts and propels the material particles along the pipeline. There are two primary types of pneumatic conveying systems: suction (or vacuum) systems and pressure systems. Suction systems operate by creating a negative pressure at the inlet, drawing material into the pipeline using a fan or vacuum pump. Pressure systems, conversely, use a positive pressure generated by a blower or compressor to push material through the pipeline. The choice between these systems depends on factors such as the distance of transport, the material's properties, and the desired system configuration.
Key Working Scenarios for Barley Pneumatic Conveying
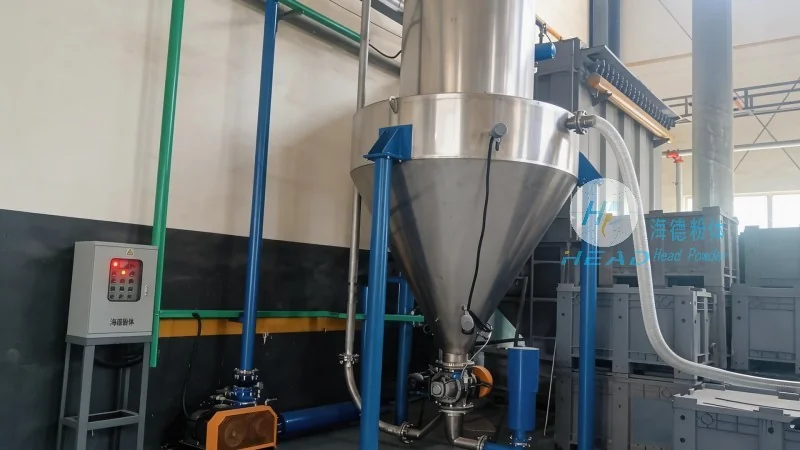
The application of pneumatic conveying in barley handling offers significant advantages over traditional methods like belt conveyors or bucket elevators. In agricultural and food processing facilities, pneumatic systems are commonly used for transferring barley from storage silos to processing lines, such as cleaning, drying, or milling. The ability to handle large volumes of barley with minimal space requirements makes this technology ideal for modern grain processing plants. Additionally, pneumatic conveying is often employed in the transportation of barley between different stages of production, ensuring a continuous and efficient flow of material. For example, in a malting facility, pneumatic systems can transport barley from storage to the malting tanks, facilitating the initial steps of the brewing process. The gentle handling of barley by pneumatic systems also minimizes material degradation, preserving the quality of the grain for subsequent processing.
Advantages of Pneumatic Conveying in Barley Handling
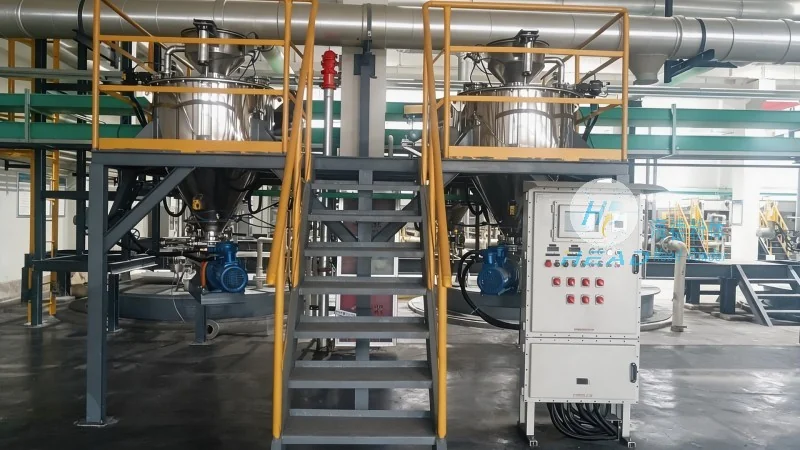
When applied to barley, pneumatic conveying systems provide several key benefits. Firstly, they offer a dust-free and enclosed transport environment, which is crucial for maintaining grain quality and preventing contamination. Unlike open systems, pneumatic conveyors keep barley particles contained within the pipeline, reducing the risk of dust exposure and improving workplace safety. Secondly, these systems are highly flexible and can be easily integrated into existing processing lines. They can be configured to handle varying flow rates and material compositions, adapting to the changing needs of barley processing operations. Thirdly, pneumatic conveying reduces labor costs and operational complexity compared to manual or mechanical handling methods. The automated nature of the system minimizes the need for manual intervention, streamlining the overall workflow and enhancing productivity. Furthermore, the energy efficiency of modern pneumatic systems, particularly when optimized for specific material characteristics, contributes to lower operational costs over time.
Customization and System Design by HeadPowder
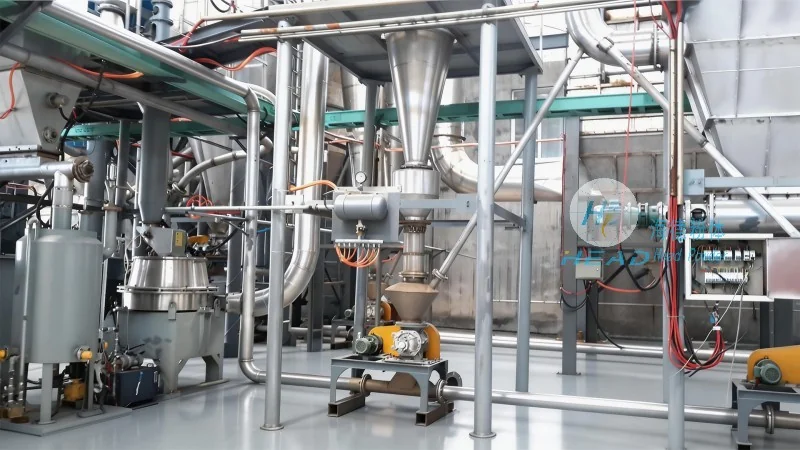
HeadPowder Engineering Co., Ltd., with its headquarters in Shandong, China, specializes in developing customized pneumatic conveying solutions tailored to the unique requirements of barley handling applications. The company's engineers work closely with clients to assess their specific needs, including the volume of barley to be transported, the distance of the transport route, and the existing infrastructure. Based on this assessment, HeadPowder designs and implements systems that optimize performance, reliability, and cost-effectiveness. The company utilizes advanced engineering software and industry best practices to ensure that each pneumatic conveying system is tailored to the specific characteristics of barley, such as its density, moisture content, and particle size distribution. This customization ensures that the system operates efficiently and maintains the quality of the barley throughout the conveying process. HeadPowder's expertise in material handling engineering, combined with its focus on client-specific solutions, makes it a trusted partner for businesses seeking reliable and efficient pneumatic conveying systems for barley and other bulk materials.




