Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field of pneumatic conveying technology, specializes in providing advanced solutions for material handling and transportation. Based in Shandong, China, the company, commonly known as HeadPowder, has established itself as a trusted partner for industries requiring efficient and reliable multi-function pneumatic conveying systems.
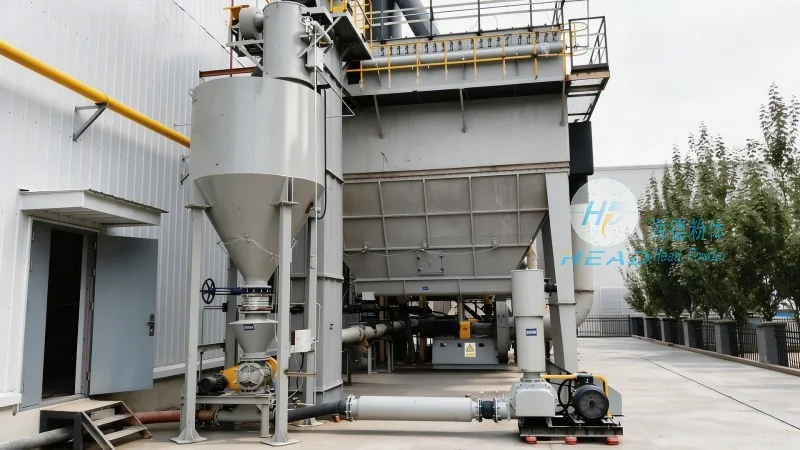
Understanding Pneumatic Conveying Systems
Pneumatic conveying systems utilize air or gas to transport bulk materials from one location to another. These systems are widely used across various industries, including food processing, pharmaceuticals, chemicals, and mining, due to their ability to handle a wide range of materials with minimal contamination and high efficiency. The core of a pneumatic conveying system lies in its ability to create a pressure differential that propels the material through a pipeline using air flow.
Key Components of a Multi-Function Pneumatic Conveying System
A typical multi-function pneumatic conveying system consists of several critical components that work in tandem to ensure smooth operation. These include the material feed hopper, which holds the bulk material; the air compressor or blower, which generates the necessary air pressure; the conveying line, which transports the material; and the discharge unit, which delivers the material to its final destination. Additional components may include filters, cyclones, and control valves to regulate the system's performance and maintain material quality.
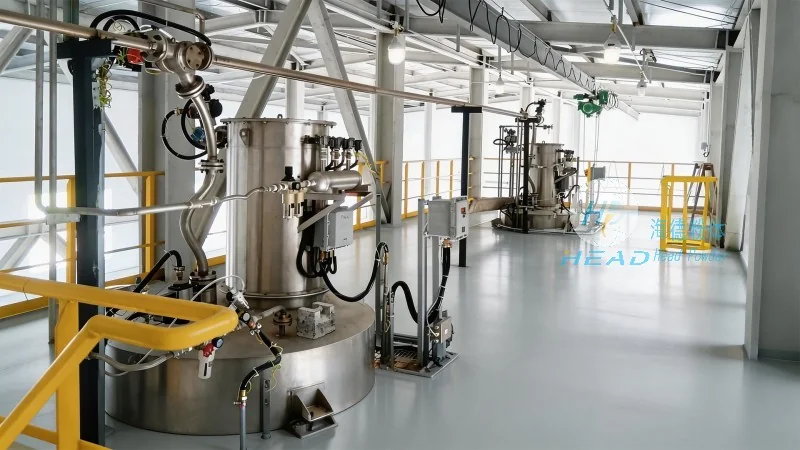
The Working Principle of Multi-Function Pneumatic Conveying
The operation of a multi-function pneumatic conveying system involves a sequence of steps that ensure the material is transported efficiently and safely. The process begins with the material being fed into the hopper. From there, the material is drawn into the conveying line by the air flow generated by the compressor. As the air and material mix, the material is suspended and propelled through the pipeline. The system's design allows for the adjustment of air pressure and flow rate to accommodate different material types and conveying distances. The discharge unit then separates the material from the air, typically using a cyclone or filter, and delivers the material to the desired location.
Operation Process: Step-by-Step Overview
The operation process of a multi-function pneumatic conveying system can be broken down into several key stages. First, the bulk material is loaded into the feed hopper. The system then starts the air compressor, which increases the air pressure within the conveying line. As the air pressure builds, the material is drawn from the hopper and into the pipeline. The material is then transported through the line, with the air flow maintaining the material's suspension. At the discharge end, the system uses a separator to remove the material from the air stream. The separated material is collected in a container, while the air is either recirculated or vented to the atmosphere. This continuous cycle allows for the efficient and reliable transport of materials over long distances.
Advantages of Multi-Function Pneumatic Conveying
Multi-function pneumatic conveying systems offer several advantages over traditional material handling methods. These include minimal material degradation due to reduced friction and impact, as the material is transported in a suspended state. The systems also provide excellent containment and hygiene, making them suitable for food and pharmaceutical applications. Additionally, the ability to handle a wide range of materials, from fine powders to bulk solids, makes these systems versatile and adaptable to various industrial needs. The systems are also relatively compact and can be integrated into existing facilities, reducing installation costs and space requirements.
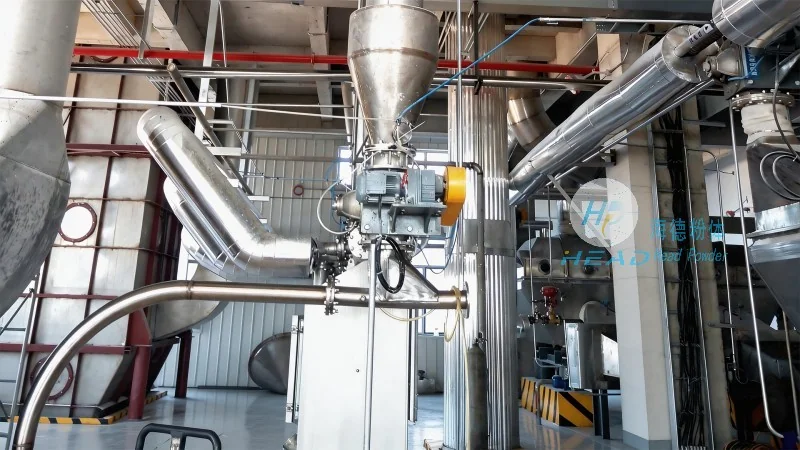
Applications and Industries Served
Multi-function pneumatic conveying systems are utilized in a variety of industries, each with specific material handling requirements. In the food industry, these systems are used to transport ingredients such as flour, sugar, and spices, ensuring minimal contamination and maintaining product quality. The pharmaceutical industry relies on these systems for the transport of active pharmaceutical ingredients (APIs) and other sensitive materials, where hygiene and purity are paramount. In the chemical industry, pneumatic conveying systems handle a wide range of chemicals, from powders to granules, while maintaining safety and environmental standards. The mining and minerals industry also benefits from these systems, as they efficiently transport raw materials and byproducts from processing plants to storage or processing facilities.
Conclusion
Shandong HeadPowder Engineering Co., Ltd. continues to innovate and provide cutting-edge multi-function pneumatic conveying solutions that meet the evolving needs of modern industries. By understanding the operation process and working principles of these systems, businesses can optimize their material handling operations, improve efficiency, and reduce costs. The company's commitment to quality and reliability ensures that its customers receive systems that are tailored to their specific requirements, delivering long-term performance and value.




