Intelligent tonne bag loading stations are advanced material handling systems engineered to efficiently receive, store, and dispense bulk materials in industrial settings. These stations are pivotal for optimizing material flow, enhancing operational efficiency, and ensuring safety across various manufacturing and processing industries. The equipment is designed to handle large capacity bags, typically 1 tonne or more, and integrates with automated material handling processes to streamline production workflows.
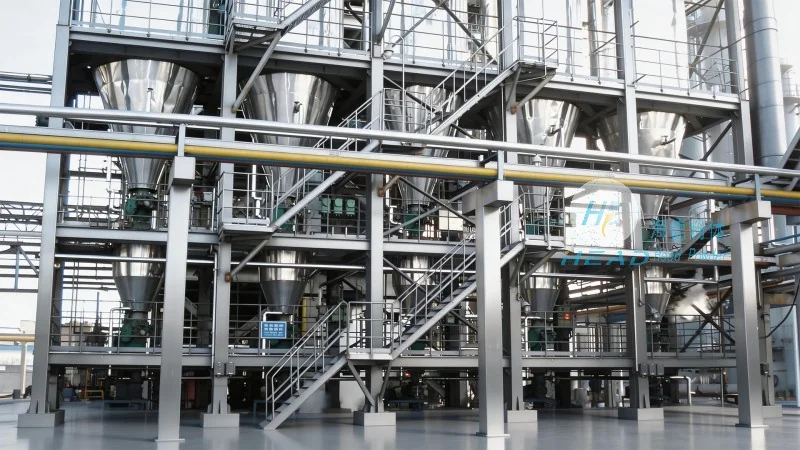
Understanding the Core Functionality of Tonne Bag Loading Stations
The primary purpose of a tonne bag loading station is to facilitate the seamless transfer of bulk materials from storage bags to downstream processing equipment. This includes functions such as bag opening, material discharge, and optional bag emptying or compaction. The system is typically equipped with sensors, actuators, and control mechanisms to automate these operations, reducing manual labor and minimizing the risk of material spillage or contamination. Key components often include a bag support frame, a discharge chute, a conveyor system, and a control panel that manages the entire process. The integration of these elements ensures that materials are handled safely and efficiently, aligning with industry standards for material handling and safety protocols.
Design Principles Behind Intelligent Material Handling Equipment
The design of intelligent tonne bag loading stations adheres to several core principles aimed at maximizing performance, reliability, and user safety. First, the equipment is built with robust construction to withstand heavy loads and harsh industrial environments. Materials such as stainless steel or high-strength polymers are commonly used for components that come into direct contact with materials, ensuring durability and resistance to corrosion. Second, the system incorporates advanced automation technologies, including programmable logic controllers (PLCs), sensors, and feedback mechanisms. These technologies enable real-time monitoring of the loading process, allowing for adjustments to be made automatically to maintain optimal performance. Third, ergonomic design is prioritized to ensure operator safety and ease of use. Features like adjustable height, clear operational indicators, and intuitive control interfaces reduce the risk of accidents and improve overall user experience. Additionally, the design emphasizes modularity, allowing for easy integration with existing production lines and future scalability as production needs evolve.
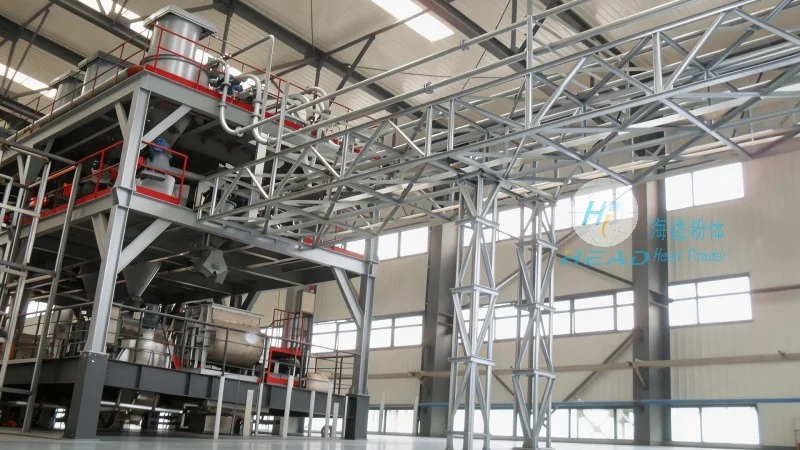
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a leading manufacturer of material handling solutions, specializes in the design, development, and production of intelligent tonne bag loading stations. With a strong presence in the industrial equipment sector, the company has built a reputation for delivering high-quality, reliable equipment tailored to the specific needs of various industries. HeadPowder's engineering team leverages years of experience and cutting-edge technology to create solutions that enhance operational efficiency and reduce costs for clients. The company's commitment to innovation and customer satisfaction is reflected in its product line, which includes a range of customizable options to meet diverse material handling requirements. HeadPowder's facilities, located in Shandong, China, are equipped with state-of-the-art manufacturing equipment and quality control systems, ensuring that each product meets stringent industry standards before delivery. By focusing on both functionality and durability, HeadPowder provides customers with equipment that not only meets current needs but also supports long-term growth and productivity.
Key Features and Benefits of Intelligent Tonne Bag Loading Stations
Intelligent tonne bag loading stations offer several key features that contribute to their effectiveness in industrial applications. These include automated bag handling, which reduces the need for manual intervention and minimizes labor costs. The integration of conveyor systems allows for the smooth transfer of materials to processing equipment, eliminating bottlenecks and improving throughput. Additionally, the stations often include features such as bag weight monitoring and material level detection, providing real-time data on inventory and process status. This information can be used to optimize production schedules and reduce downtime. Another significant benefit is the enhanced safety provided by the automated system, which minimizes the risk of accidents associated with manual handling of heavy bags. The equipment is also designed to be energy-efficient, reducing operational costs and environmental impact. Overall, the intelligent design of these stations ensures that they are not only effective in handling bulk materials but also contribute to a safer, more efficient, and sustainable industrial operation.
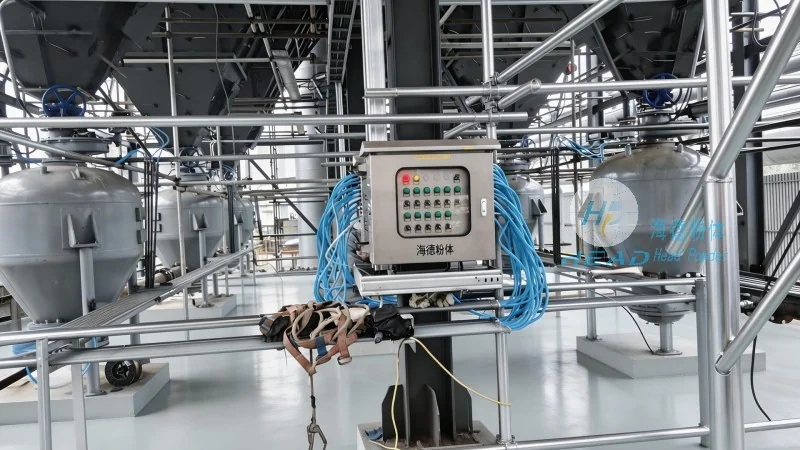
Applications and Industries Served by Tonne Bag Loading Stations
Tonne bag loading stations are widely used across various industries that handle bulk materials. Common applications include the chemical, food processing, pharmaceutical, and mining sectors. In the chemical industry, these stations are used to handle raw materials such as powders and granules, ensuring safe and efficient transfer to reactors and processing equipment. The food processing industry benefits from the hygienic design of the equipment, which meets strict sanitation standards and prevents contamination of food products. In the pharmaceutical sector, the stations are used to handle active ingredients and other materials, with features like dust control and contamination prevention being critical. The mining industry utilizes these systems to handle bulk materials such as ores and minerals, improving the efficiency of material handling in mining operations. Regardless of the industry, the intelligent design of tonne bag loading stations ensures that they can be adapted to meet the specific requirements of each application, providing a versatile solution for material handling needs.
Conclusion: The Role of Intelligent Tonne Bag Loading Stations in Modern Manufacturing
In conclusion, intelligent tonne bag loading stations represent a significant advancement in material handling technology, offering enhanced efficiency, safety, and reliability in industrial operations. The design principles behind these systems, including robust construction, advanced automation, and ergonomic considerations, ensure that they can meet the demands of modern manufacturing environments. As industries continue to evolve and seek more efficient and sustainable solutions, the role of intelligent material handling equipment like tonne bag loading stations will only become more critical. Companies like Shandong HeadPowder Engineering Co., Ltd. play a vital role in providing these advanced solutions, helping businesses optimize their operations and stay competitive in a rapidly changing market. By investing in intelligent tonne bag loading stations, industries can improve productivity, reduce costs, and enhance overall operational performance, contributing to long-term success and growth.




