Coal fly ash pneumatic conveying machines are advanced industrial equipment designed to transport coal fly ash efficiently and safely. This equipment operates based on the principle of pneumatic conveying, which utilizes air flow to move particulate materials like coal fly ash through a pipeline system. The core mechanism involves creating a pressure differential between the conveying line and the ambient environment, enabling the ash particles to be suspended and transported by the air stream. This method offers significant advantages over traditional mechanical conveying systems, such as reduced wear and tear on components, lower maintenance requirements, and the ability to handle materials in a dust-free environment.
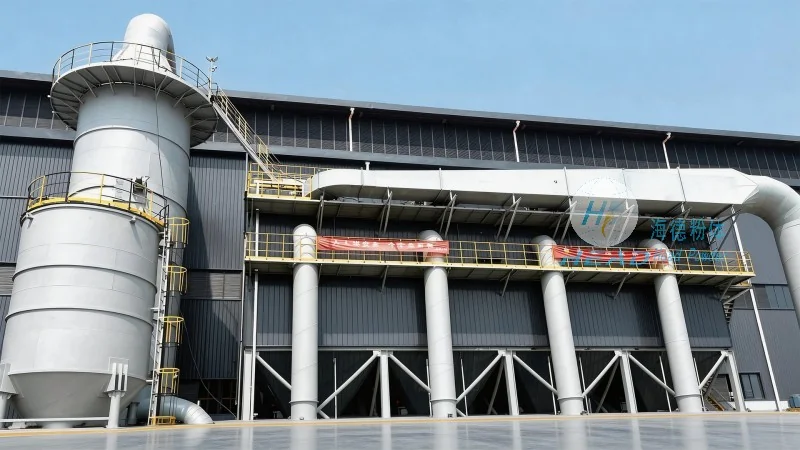
Working Principle of Coal Fly Ash Pneumatic Conveying Machines
The fundamental principle of coal fly ash pneumatic conveying is the use of air as a carrier medium to transport fine particulate materials. The system typically consists of a blower or compressor that generates the necessary air pressure, a hopper for material storage, a conveying line, and a receiver for the discharged material. As the ash is fed into the hopper, the air is introduced, creating a flow that lifts and transports the particles. The velocity of the air is critical; it must be sufficient to keep the ash in suspension but not so high as to cause excessive pressure drops or energy consumption. The design of the conveying line, including bends and fittings, is optimized to minimize pressure loss and ensure smooth material flow. This pneumatic approach effectively prevents dust contamination and allows for long-distance transport of coal fly ash from power plants or other industrial sources to storage or disposal sites.
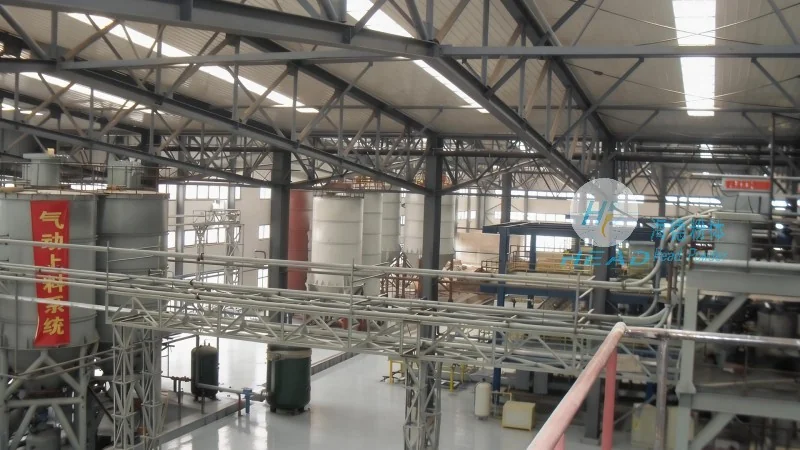
Key Working Scene Characteristics
Coal fly ash pneumatic conveying machines are widely used in industrial settings where the handling of fine particulate materials is essential. Their application scenarios are diverse and tailored to specific operational needs. One primary use case is in thermal power plants, where coal fly ash is generated as a byproduct of coal combustion. The equipment efficiently transports the ash from the boiler to storage silos or for further processing, such as cement production or road construction. Another common application is in industrial facilities that process or utilize coal fly ash as a raw material, such as in the manufacturing of building materials or as a filler in concrete. The flexibility of pneumatic conveying allows these machines to operate in various environments, from indoor processing plants to outdoor storage facilities, adapting to different site layouts and material flow requirements.
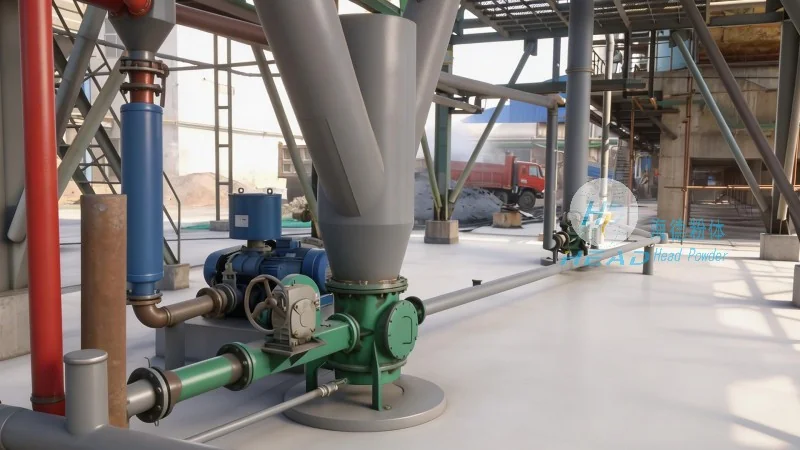
Advantages in Specific Work Environments
In industrial work environments, the characteristics of coal fly ash pneumatic conveying machines make them particularly suitable for applications where traditional methods are inadequate. For instance, in power plants, the need to handle large volumes of ash while maintaining environmental standards drives the adoption of these systems. The dust-free operation of pneumatic conveying reduces the risk of air pollution and occupational health hazards, aligning with modern industrial safety regulations. Additionally, the ability to transport ash over long distances without the need for intermediate storage or handling points simplifies logistics and reduces operational costs. In construction and material processing industries, the use of coal fly ash as a supplementary cementitious material (SCM) requires reliable and efficient transport systems. Pneumatic conveying machines meet these demands by providing consistent material flow and minimizing material degradation during transport. The adaptability of these systems to different ash compositions and particle sizes further enhances their utility in various work environments.
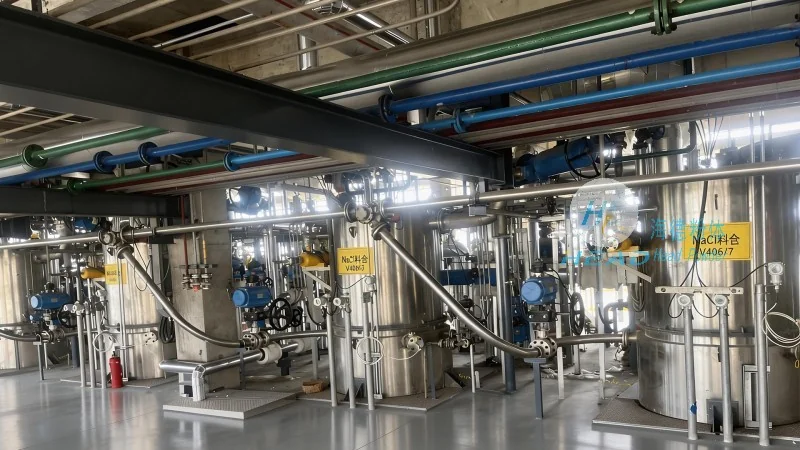
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, specializes in the design, manufacturing, and supply of industrial conveying equipment, including coal fly ash pneumatic conveying machines. The company is headquartered in Shandong, China, and has established itself as a leading provider of advanced material handling solutions for the coal and power industries. With a focus on innovation and customer-centric design, headpowder develops equipment tailored to the specific needs of its clients, ensuring high efficiency, reliability, and durability. The company’s products are engineered to meet international standards and are widely recognized for their performance in demanding industrial applications. By leveraging years of experience and technical expertise, headpowder continues to enhance its product line to meet the evolving requirements of the market, providing sustainable and effective solutions for coal fly ash management and transportation.




