For industrial operations dealing with potash fertilizer, efficient material handling is crucial. Pneumatic conveying equipment, specifically designed for potash fertilizer, offers a reliable solution that enhances productivity and safety in material transport. This article explores the fundamental principles and operational characteristics of such systems, highlighting their role in modern fertilizer processing and handling.
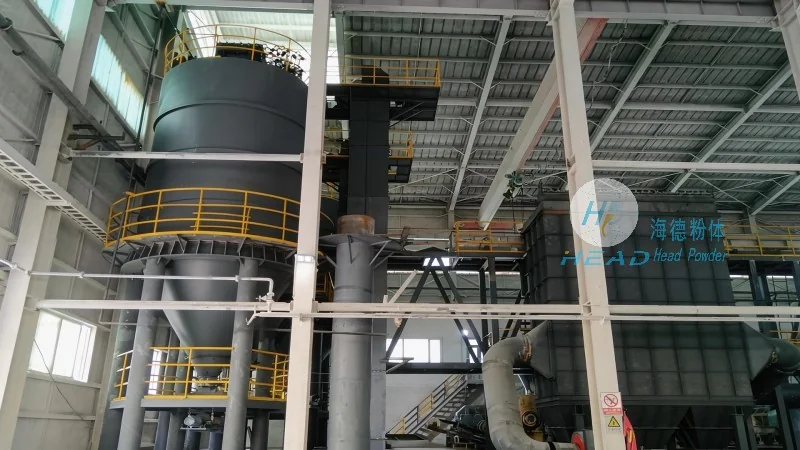
The Working Principle of Pneumatic Conveying Systems for Potash Fertilizer
The core principle of potash fertilizer pneumatic conveying systems is the use of air pressure to move bulk materials through a pipeline network. Unlike traditional mechanical conveyors, which rely on physical contact and moving parts, pneumatic systems utilize air as the primary medium to transport the fertilizer. The process typically involves generating a high-pressure air stream, which draws the potash fertilizer particles into the pipeline. As the air flows through the system, it carries the material to the desired destination, such as storage silos, processing units, or packaging areas. This method eliminates the need for mechanical components like belts or buckets, reducing maintenance requirements and minimizing the risk of material contamination.
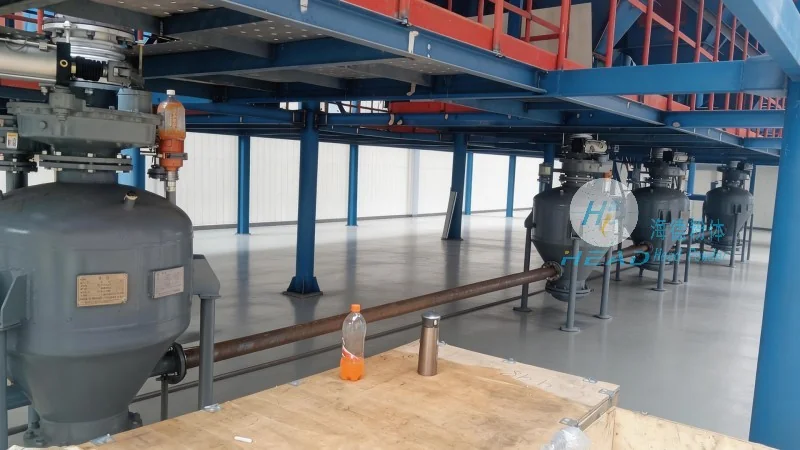
Key Components and Their Functions in the System
Several critical components work together to ensure the smooth operation of a potash fertilizer pneumatic conveying system. The primary components include the air compressor, which generates the necessary air pressure; the material feeder, which controls the flow of fertilizer into the system; the conveying line, which transports the material; and the receiver, where the fertilizer is deposited. Additionally, accessories like filters, cyclones, and pressure regulators are essential for maintaining system efficiency and preventing air leakage or material blockages. Each component is carefully designed to handle the specific characteristics of potash fertilizer, such as its granular size, moisture content, and potential for dust generation.
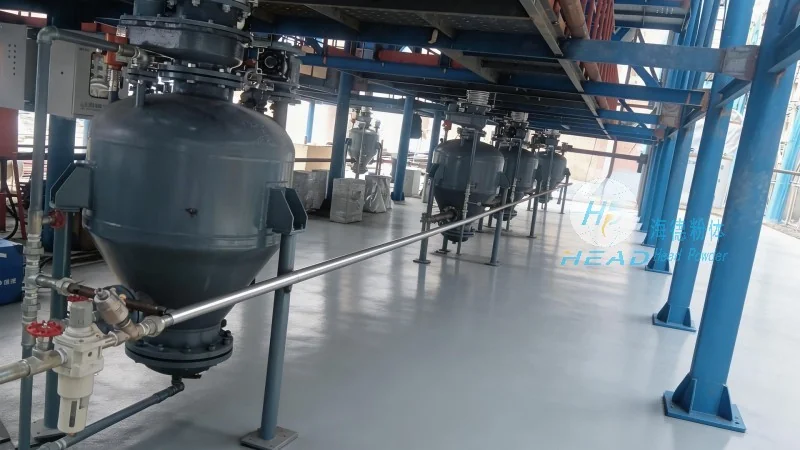
Working Scene Characteristics and Application Scenarios
The working scene characteristics of potash fertilizer pneumatic conveying equipment are tailored to the demands of fertilizer production and handling environments. These systems are commonly used in large-scale fertilizer plants, where bulk quantities of potash fertilizer need to be moved between processing stages. The equipment is designed to operate in both indoor and outdoor settings, with options for enclosed or open-air configurations depending on the facility layout. Key characteristics include high capacity, allowing for the transport of large volumes of material in a short time, and flexibility in routing, as the conveying lines can be easily reconfigured to adapt to changing production needs. Furthermore, the systems are built to withstand the corrosive and abrasive nature of potash fertilizer, ensuring long-term durability and minimal downtime.
Technical Advantages and Practical Applications
Technological advancements have enhanced the efficiency and reliability of potash fertilizer pneumatic conveying systems. Modern systems incorporate features like variable speed drives, which allow for precise control of air pressure and material flow, optimizing energy consumption and reducing operational costs. The use of high-quality materials, such as stainless steel or specialized coatings, protects the equipment from corrosion and wear, extending its service life. These systems also offer improved safety features, including dust suppression mechanisms and emergency shut-off valves, which minimize the risk of accidents and ensure compliance with industrial safety standards. In practical applications, the equipment is widely used in the fertilizer industry for transporting potash from storage to processing units, as well as for packaging and distribution. The ability to handle large volumes of material with minimal human intervention makes it an ideal solution for high-throughput operations.
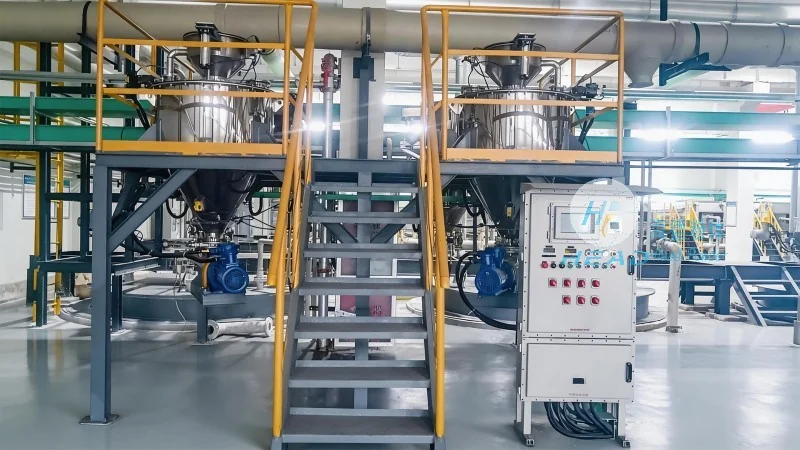
Conclusion and Company Profile
In conclusion, potash fertilizer pneumatic conveying equipment represents a sophisticated and efficient solution for material handling in the fertilizer industry. By leveraging the principles of pneumatic transport, these systems enhance productivity, reduce operational costs, and improve safety in fertilizer processing. The technology is designed to meet the specific demands of potash fertilizer, offering high capacity, flexibility, and durability. As a leading manufacturer in this field, Shandong HeadPowder Engineering Co., Ltd. specializes in providing customized pneumatic conveying solutions tailored to the needs of fertilizer producers. With a focus on quality and innovation, the company ensures that its equipment meets the highest standards of performance and reliability, supporting the efficient operation of fertilizer facilities worldwide.




