Quartz powder, a widely used industrial material, often requires efficient and reliable transport solutions for various applications. The quartz powder pneumatic conveying machine is a specialized equipment designed to handle the transportation of quartz powder through an air-driven system. This article explores the fundamental principles behind its operation and the specific working scene characteristics that define its effectiveness in industrial settings.
About HeadPowder: Your Trusted Partner in Pneumatic Conveying Solutions
HeadPowder, operating as Shandong HeadPowder Engineering Co., Ltd., is a leading manufacturer based in Shandong, China. With a focus on delivering high-quality pneumatic conveying equipment, the company specializes in customizing solutions tailored to the unique needs of industries handling fine powders like quartz. The expertise and innovation of HeadPowder ensure that clients receive equipment that meets stringent performance and safety standards.
The Core Principle of Quartz Powder Pneumatic Conveying
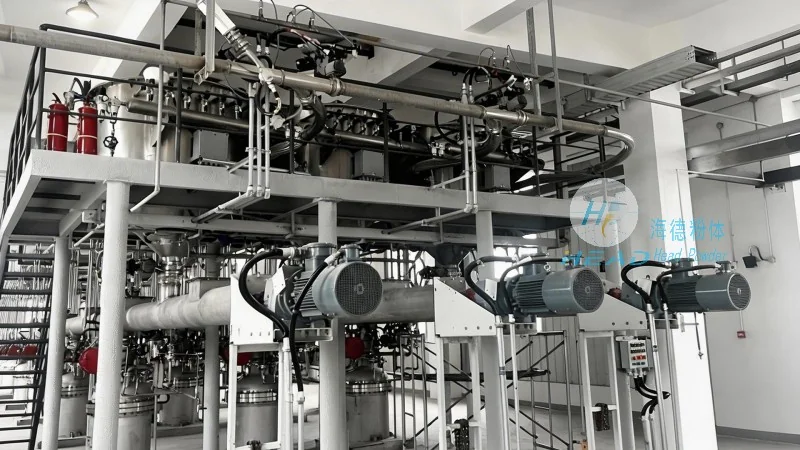
The operation of a quartz powder pneumatic conveying machine is based on the fundamental principle of air movement to transport solid particles. The system typically consists of a hopper for material storage, a blower or compressor to generate airflow, and a pipeline network that guides the powder from the source to the destination. As quartz powder is fed into the system, the air flow creates a suspension of the powder particles, allowing them to be carried through the pipeline. This process, known as pneumatic conveying, eliminates the need for mechanical components like belts or buckets, reducing maintenance and operational costs.
Working Scene Characteristics of Quartz Powder Pneumatic Conveying Machines
The effectiveness of quartz powder pneumatic conveying machines is heavily influenced by the working scene characteristics, which include the particle size, moisture content, and flow rate of the quartz powder. In industrial applications, these machines are often used in environments where dust control and material handling efficiency are critical. For instance, in mining and processing facilities, the equipment is employed to transport quartz powder from storage silos to processing units, ensuring a continuous and clean operation. The working scene also considers the distance and layout of the transport path, as the design of the pipeline and air flow velocity must be optimized to prevent particle segregation or blockages. Additionally, the system's ability to handle varying material loads and maintain consistent airflow is crucial for maintaining operational stability in dynamic industrial settings.
Key Advantages and Practical Applications
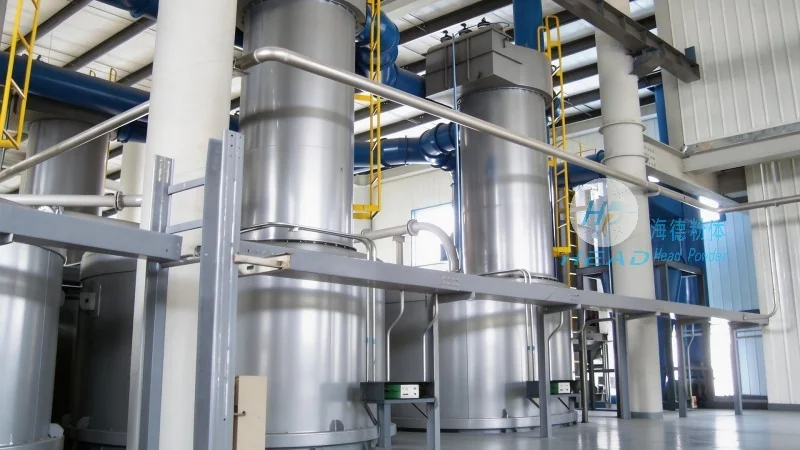
Quartz powder pneumatic conveying machines offer several advantages over traditional mechanical conveying methods. The primary benefit is the reduction in labor and maintenance costs, as the system operates with minimal moving parts. Furthermore, the enclosed pipeline design helps in controlling dust emissions, which is essential for maintaining a safe and healthy working environment. In industries such as ceramics, glass manufacturing, and construction materials, the equipment is widely used to transport quartz powder due to its ability to handle fine particles without degradation. The working scene characteristics, such as the need for high-purity materials, are well-addressed by these systems, as they prevent contamination from external sources. HeadPowder's expertise in designing and manufacturing these machines ensures that clients receive solutions that are tailored to their specific operational requirements, enhancing productivity and reducing downtime.




