HeadPowder, a leading provider of industrial conveying solutions, specializes in advanced pneumatic conveying systems designed for efficient handling of fine coal powders. Based in Shandong, China, the company has established itself as a trusted partner in the energy and processing industries, delivering reliable equipment that meets the demands of modern material transport. This article explores the fundamental principles behind fine coal powder pneumatic conveying machines and highlights the key working scene characteristics that define their application in various industrial settings.
Company Overview and Expertise
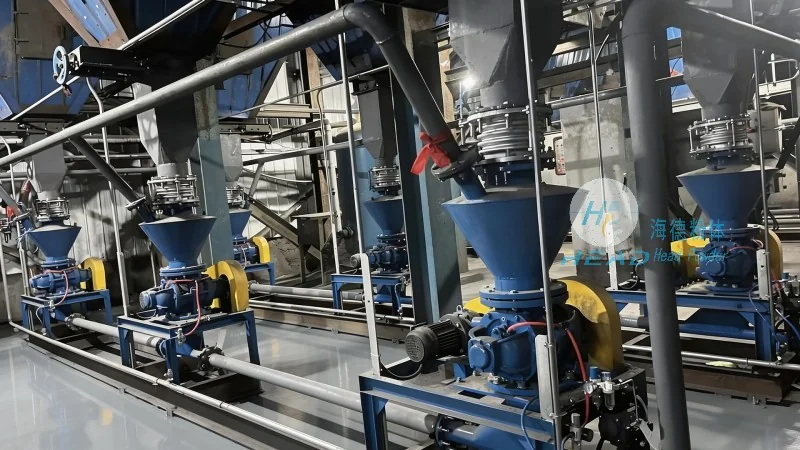
Shandong HeadPowder Engineering Co., Ltd. (HeadPowder) is a professional manufacturer and supplier of pneumatic conveying equipment. With a strong focus on innovation and customer satisfaction, HeadPowder has built a reputation for producing high-quality systems tailored to the unique requirements of coal processing, power generation, and related industries. The company’s headquarters is located in Shandong, China, where its research and development team continuously optimizes existing technologies and develops new solutions to enhance operational efficiency and safety in material handling processes.
The Principle of Fine Coal Powder Pneumatic Conveying
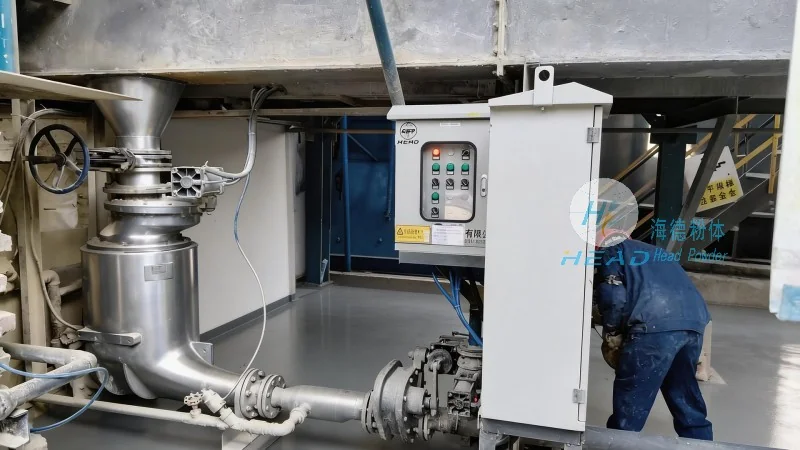
Fine coal powder pneumatic conveying machines operate on the principle of transporting particulate materials through a pipeline using a stream of air or other gas. The system typically consists of a hopper, a feeder, a conveying line, and a receiver. The process begins with the coal powder being fed into the hopper, where it is then drawn into the conveying line by a vacuum or pressure created by the air mover. The air flow carries the fine particles through the pipeline to the destination point, such as a storage silo or processing unit. This method eliminates the need for mechanical components like belts or buckets, reducing maintenance costs and minimizing the risk of material contamination. The key to efficient operation lies in maintaining the correct air-to-material ratio, which ensures that the particles are fully suspended and transported without clogging or degradation.
Working Scene Characteristics of Fine Coal Powder Pneumatic Conveying Machines
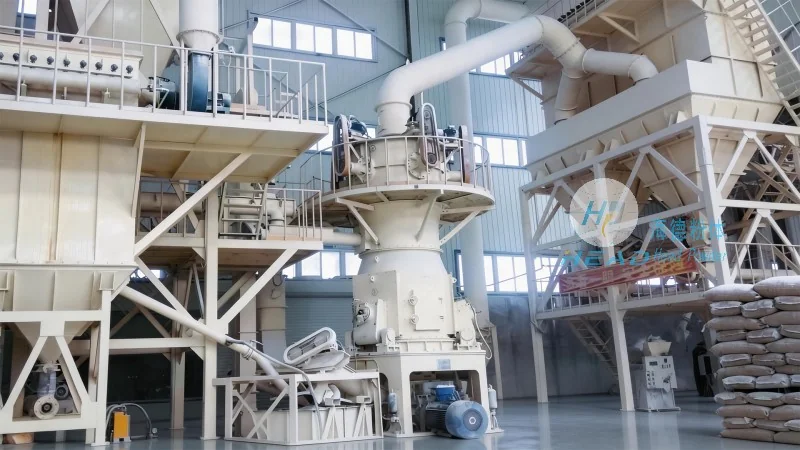
The application of fine coal powder pneumatic conveying machines is characterized by several distinct working scene features that make them ideal for specific industrial environments. Firstly, these systems are particularly suited for handling fine, dusty materials that are prone to caking or agglomeration when exposed to moisture or air. The enclosed pipeline design prevents dust from escaping into the environment, ensuring compliance with environmental regulations and maintaining a safe working atmosphere. Secondly, the flexibility of pneumatic conveying allows for the integration of multiple feeding and receiving points within a single system, enabling complex material flow paths that adapt to changing production schedules. This adaptability is crucial in power plants and coal processing facilities where material is transported from storage to boilers or other processing equipment. Thirdly, the system’s ability to operate under both vacuum and pressure modes provides versatility in handling materials with varying properties, such as different coal grades or moisture content. This dual-mode capability ensures that the conveying process remains efficient even when dealing with challenging materials that require specific transport conditions.
Key Advantages and Practical Applications
Fine coal powder pneumatic conveying machines offer several advantages that make them a preferred choice in industrial applications. One of the primary benefits is the reduction in material handling time and labor costs, as the automated system minimizes the need for manual intervention in the transport process. Additionally, the enclosed design reduces dust exposure for operators, improving workplace safety and reducing the risk of respiratory issues associated with fine particulate handling. The system also contributes to energy efficiency by using compressed air or vacuum systems that are optimized for the specific material being conveyed, resulting in lower operational costs over the long term. In practical applications, these machines are commonly used in coal-fired power plants to transport coal from storage silos to boilers, in coal preparation plants to move raw coal to processing units, and in industrial facilities that require the transfer of fine powders for further processing. The reliability and durability of the equipment, combined with the company’s after-sales support, ensure that clients can rely on consistent performance and minimal downtime.
Conclusion and Future Outlook
As industrial processes continue to demand more efficient and sustainable material handling solutions, fine coal powder pneumatic conveying machines remain a critical component in the energy and processing sectors. HeadPowder’s commitment to innovation and quality ensures that their products meet the evolving needs of the industry, providing reliable and efficient conveying solutions for clients worldwide. By understanding the principles and working scene characteristics of these systems, businesses can make informed decisions about implementing pneumatic conveying technology to enhance their operational efficiency and safety. With its headquarters in Shandong, China, HeadPowder continues to lead the way in developing advanced conveying solutions that address the challenges of modern industrial material transport.




