High temperature fine powder material handling systems are critical components in industrial processes that involve the transportation of hot, fine particulate materials. These systems are designed to efficiently and safely transport materials such as cement, coal ash, and other high-temperature powders over long distances while maintaining material integrity and operational efficiency. The core of these systems lies in their specialized equipment and the principles that govern their operation, which are tailored to handle the unique challenges posed by high-temperature environments.
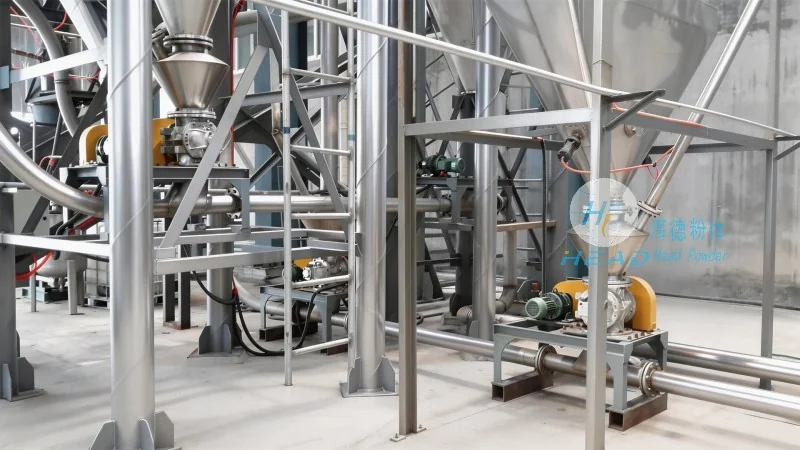
Company Overview
HeadPowder, a leading manufacturer in the field, specializes in the design, development, and supply of advanced material handling solutions. With a strong presence in Shandong, China, the company leverages over years of industry experience to deliver high-quality equipment tailored to the specific needs of clients in various sectors, including cement production, power generation, and chemical processing. The company's commitment to innovation and customer satisfaction has established it as a trusted partner for businesses seeking reliable and efficient material handling systems.
Principle of High Temperature Fine Powder Material Handling Systems
The operation of high temperature fine powder material handling systems is based on several key principles that ensure effective and safe material transport. One of the primary principles is the use of specialized conveyor technologies, such as pneumatic conveying systems and mechanical screw conveyors, which are engineered to handle high-temperature materials without compromising performance. Pneumatic conveying systems, for instance, utilize air pressure to move powders through pipelines, while mechanical screw conveyors use rotating screws to push materials forward. Both methods are adapted to withstand high temperatures, often incorporating heat-resistant materials and insulation to protect components from thermal stress.
Another critical principle is the integration of temperature control mechanisms. These systems are equipped with sensors and control systems that monitor and regulate the temperature of the material and the equipment itself. This ensures that the material remains in a stable state during transport, preventing issues such as clumping or degradation that can occur with high-temperature powders. Additionally, the design of the system includes features like airlocks and dust collection systems to maintain a safe working environment and comply with environmental regulations.
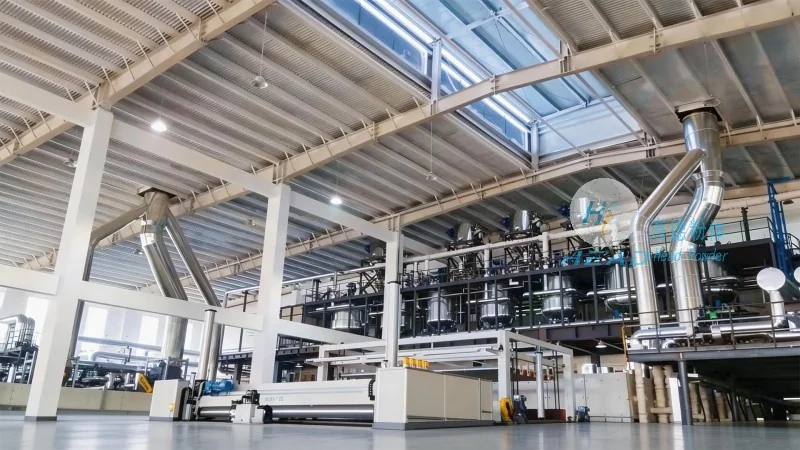
Working Scene Characteristics
The working scene characteristics of high temperature fine powder material handling systems vary significantly based on the application and the environment in which they are used. In cement plants, for example, these systems are typically used to transport hot clinker and raw materials between different processing stages. The high temperatures involved, often exceeding 200°C, require specialized equipment that can withstand continuous exposure to heat and abrasive materials. The systems are designed to operate continuously with minimal downtime, ensuring smooth production flow.
In power generation facilities, especially those using coal-fired boilers, high temperature fine powder material handling systems are essential for transporting fly ash and bottom ash from the boiler to storage or disposal areas. The systems must handle large volumes of material at high temperatures while maintaining efficiency and safety. The working environment in these facilities is often characterized by high humidity and dust, making the durability and reliability of the equipment crucial for operational success.
In chemical processing plants, the systems may be used to transport various fine powders, such as chemicals or catalysts, at elevated temperatures. The working scene in these applications is typically more controlled, with strict quality and safety requirements. The systems are designed to minimize material loss and contamination, ensuring that the powders remain pure and effective for their intended use. The integration of automation and monitoring systems in these setups enhances operational efficiency and reduces the risk of human error.
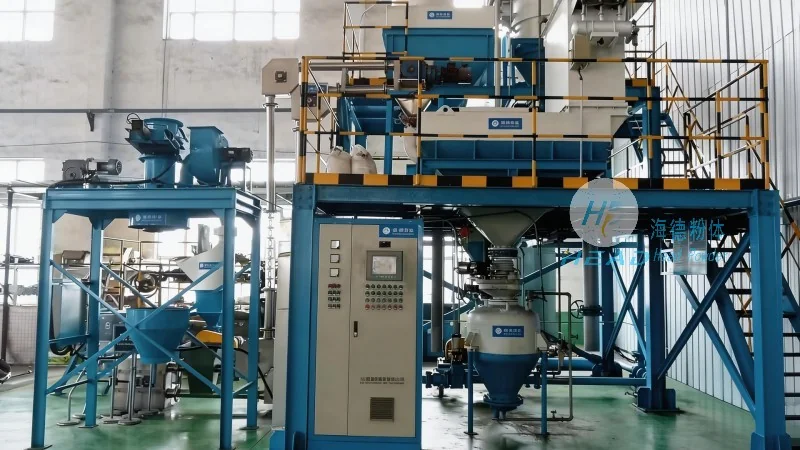
Key Features and Advantages
High temperature fine powder material handling systems offered by HeadPowder feature several advantages that make them ideal for demanding industrial applications. The equipment is designed with high-temperature resistant materials, such as stainless steel and special alloys, which can withstand continuous exposure to temperatures up to 400°C or higher. This ensures long service life and minimal maintenance requirements. The systems also incorporate advanced control systems that allow for precise regulation of material flow and temperature, enhancing operational efficiency and reducing energy consumption.
Another key advantage is the ability to handle a wide range of particle sizes and material types. The systems are adaptable to different applications, from fine powders to coarse granules, making them versatile solutions for various industrial needs. The integration of dust collection and filtration systems ensures compliance with environmental regulations and maintains a clean working environment. Additionally, the systems are designed for easy maintenance and repair, with modular components that can be replaced quickly, minimizing downtime and operational costs.
Conclusion
High temperature fine powder material handling systems are essential for efficient and safe material transport in various industrial sectors. The principles and working scene characteristics of these systems are tailored to handle the unique challenges posed by high-temperature environments, ensuring optimal performance and reliability. HeadPowder, with its expertise and commitment to quality, provides advanced solutions that meet the specific needs of clients, contributing to improved operational efficiency and productivity in industrial processes.




