HeadPowder, a leading engineering company based in Shandong, China, specializes in the design, manufacturing, and installation of advanced material handling systems. This article delves into the core principles and operational characteristics of coal and stone powder material handling equipment, highlighting how these systems efficiently transport bulk materials in industrial settings.
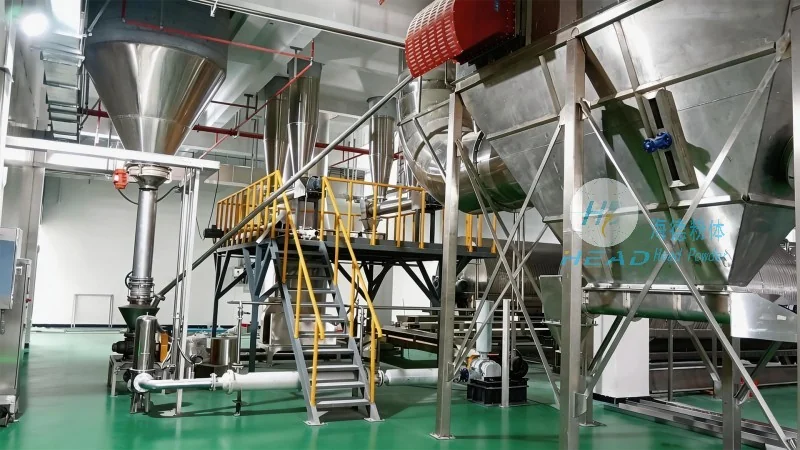
Core Principles of Coal and Stone Powder Material Handling Systems
The coal and stone powder material handling system is engineered to address the unique challenges of transporting fine and abrasive powders, such as coal dust, limestone powder, and other industrial minerals. The system typically comprises several key components, including feeders, conveyors, and control systems, all working in tandem to ensure smooth and reliable material flow. The feeding mechanism, often a screw feeder or a vibrating feeder, accurately meters the material into the conveyor, while the conveyor itself—commonly a belt or screw conveyor—transports the material to its destination. Control systems, equipped with sensors and automation technology, monitor the system's performance, adjusting parameters like speed and pressure to maintain optimal operation. This integrated approach ensures that the material is handled with minimal degradation, preventing issues like caking or blockage that can occur with traditional methods.
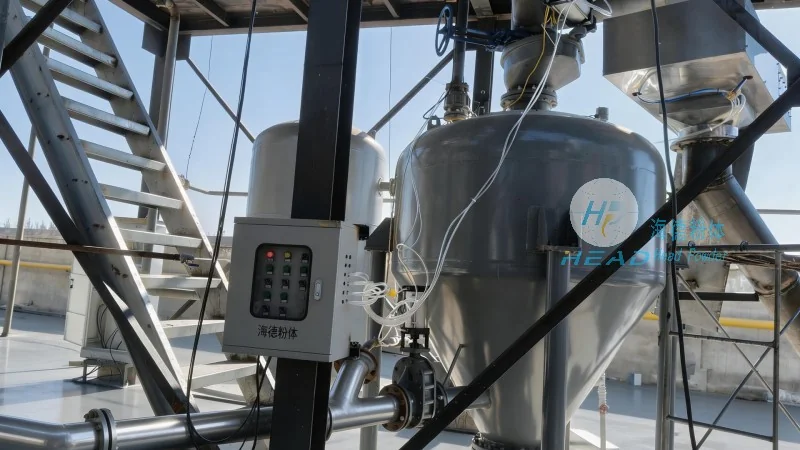
Working Scene Characteristics and Application Scenarios
The coal and stone powder material handling system is widely used across various industrial sectors, each presenting distinct operational requirements. In the coal mining industry, these systems are crucial for transporting raw coal from mines to processing facilities, where the material is prepared for combustion or further processing. The system's ability to handle high volumes of coal efficiently, while maintaining low maintenance costs, makes it an ideal solution for large-scale mining operations. In the cement and construction industries, limestone powder is a key raw material, and the material handling system ensures that this fine powder is transported to production lines without loss or contamination. The system's design, with its robust construction and dust control features, is particularly suited for environments where dust suppression is critical to safety and compliance. Additionally, in power generation plants, coal and stone powder systems play a vital role in supplying fuel to boilers, where consistent material flow is essential for stable power output. The adaptability of these systems to different material types and operational conditions makes them versatile tools for modern industrial applications.
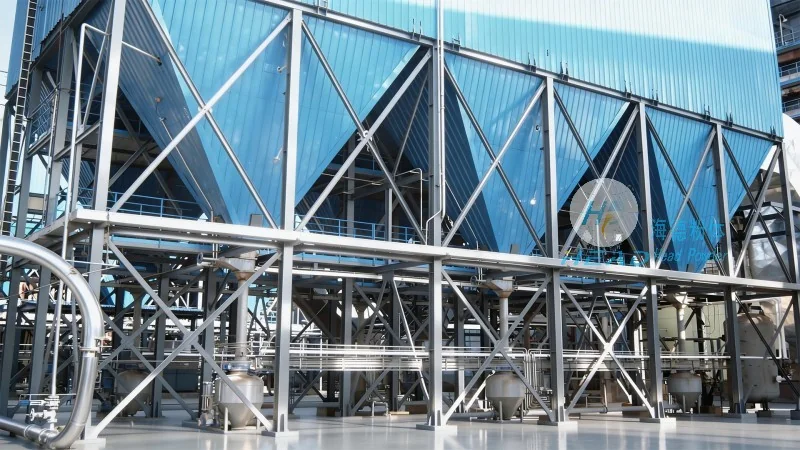
Advantages and Technical Features
HeadPowder's coal and stone powder material handling systems offer several advantages that enhance operational efficiency and reduce costs. The systems are designed with durability in mind, using high-quality materials and robust construction to withstand the harsh conditions of industrial environments. This reduces the need for frequent maintenance and repairs, leading to lower long-term operational expenses. The automation features, including real-time monitoring and predictive maintenance, further improve system reliability and minimize downtime. Additionally, the systems are equipped with dust control mechanisms, such as sealed enclosures and air filtration systems, which help maintain a safe and clean working environment. The ability to handle a wide range of particle sizes and material densities makes these systems suitable for diverse applications, from small-scale processing plants to large industrial facilities. Overall, the coal and stone powder material handling system from HeadPowder is a reliable and efficient solution for bulk material transport, meeting the demands of modern industrial operations.




