HeadPowder, a leading provider in the field of material handling solutions, specializes in air-driven transport systems for various granular materials, including borax. This article delves into the fundamental principles behind air-driven transport technology and explores the key characteristics of its application scenarios, particularly for borax granular materials.
Understanding the Principle of Air-Driven Transport for Borax Granular Materials
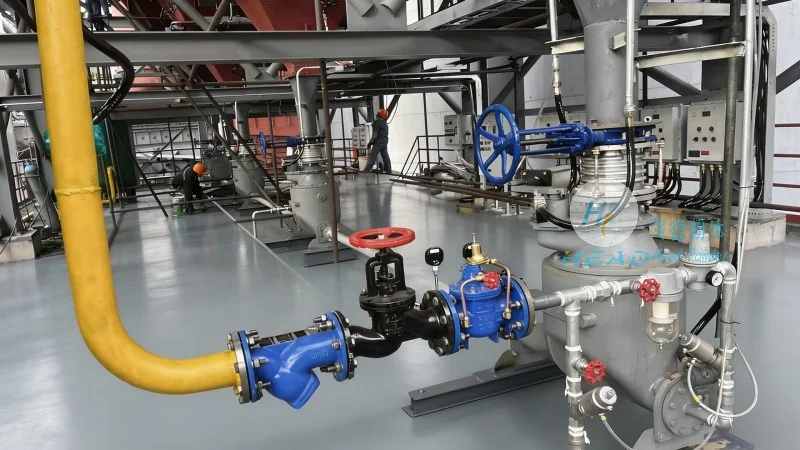
The core principle of air-driven transport, also known as pneumatic conveying, involves the use of compressed air to move solid particles through a pipeline. In the case of borax granular materials, which are typically fine to medium-sized particles with specific physical properties, this method offers several advantages over traditional mechanical conveying. The process begins with the material being fed into a hopper or feeder, where it is then drawn into a pipeline by the pressure differential created by the compressed air. The air acts as a carrier, suspending the borax particles and transporting them to the destination point. This method is particularly effective for borax due to its relatively low moisture content and moderate particle size, which allows for efficient suspension and minimal blockage in the pipeline.
Key Working Scene Characteristics of Air-Driven Transport for Borax
When applied to borax granular materials, air-driven transport systems exhibit distinct characteristics that make them suitable for specific working environments. Firstly, the system's ability to handle fine particles without significant degradation or segregation is crucial. Borax particles, being relatively uniform in size, benefit from the consistent airflow that maintains particle integrity during transport. Secondly, the system's flexibility in terms of layout and integration with existing production lines is a significant advantage. Air-driven transport can be easily adapted to different plant configurations, allowing for seamless integration with other processing equipment. Thirdly, the system's low maintenance requirements and energy efficiency contribute to operational cost savings, which is vital for industrial applications involving borax. Additionally, the enclosed nature of the pipeline system ensures minimal dust emission, aligning with environmental regulations and improving workplace safety.
Application Scenarios and Operational Benefits
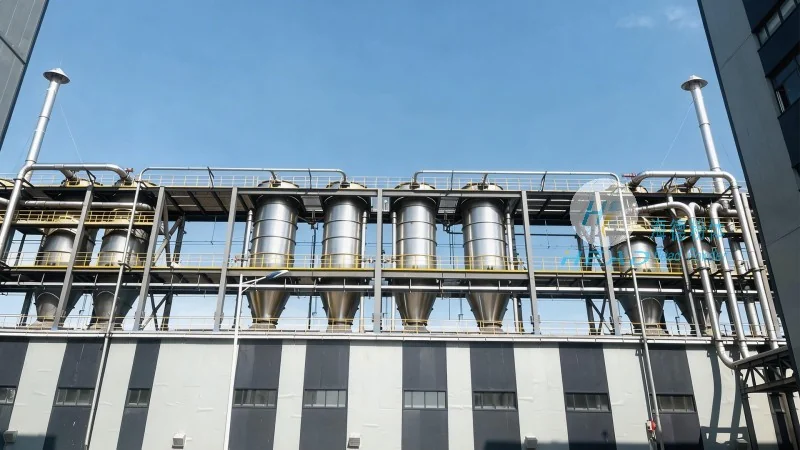
HeadPowder's air-driven transport solutions for borax granular materials are widely used in various industrial settings. One common application is in the chemical processing industry, where borax is used as a raw material in the production of detergents, glass, and other chemical products. The transport system efficiently moves borax from storage silos to processing units, ensuring a continuous supply without interruptions. Another scenario involves the pharmaceutical industry, where borax is used as an excipient or raw material in the formulation of medications. The air-driven system maintains the purity and consistency of the borax particles, which is critical for pharmaceutical applications. Furthermore, in the food and beverage industry, borax may be used as a processing aid, and the transport system ensures that the material is handled hygienically and efficiently. The operational benefits of these systems include reduced labor costs due to automated feeding and transport, increased production throughput, and improved product quality through consistent particle handling.
Technical Considerations and System Design
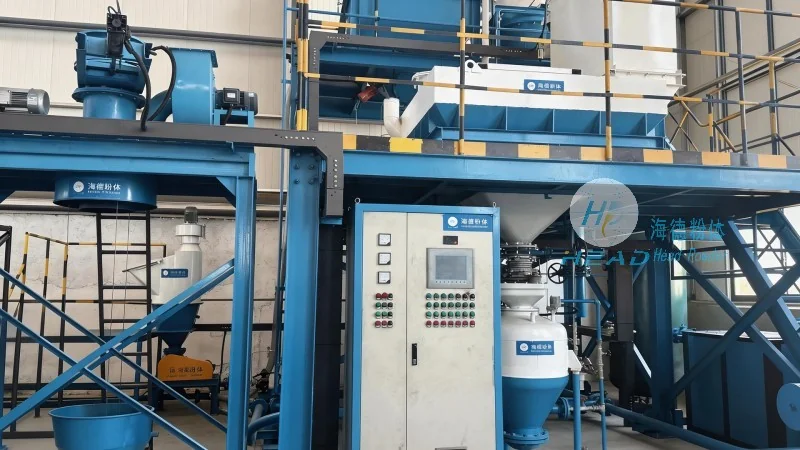
Designing an effective air-driven transport system for borax granular materials requires careful consideration of several technical factors. The choice of pipeline material, such as stainless steel or PVC, is influenced by the chemical properties of borax and the need for corrosion resistance. The diameter and length of the pipeline are optimized to balance the air velocity required for particle suspension with energy consumption. The air pressure and flow rate are carefully calibrated to ensure that the borax particles are fully suspended without causing excessive wear on the system components. HeadPowder's engineers utilize advanced computational fluid dynamics (CFD) simulations to model the transport process and optimize system parameters for maximum efficiency. Additionally, the inclusion of features like pulse jets or rotary valves helps to prevent particle buildup and maintain consistent airflow, further enhancing system reliability.
Conclusion and Company Overview
HeadPowder Engineering Co., Ltd., based in Shandong, China, is a trusted partner for businesses seeking reliable air-driven transport solutions for borax granular materials. With a focus on innovation and customer-centric design, the company provides tailored systems that meet the specific needs of industrial applications. The principles and characteristics of air-driven transport, as outlined in this article, demonstrate the effectiveness of this technology in improving operational efficiency and product quality. By leveraging the expertise of HeadPowder's team, industries can achieve seamless material handling, reduced costs, and enhanced safety in their borax processing operations.




