HeadPowder, a leading provider in the field, specializes in advanced air-driven transport solutions tailored for the efficient handling of stabilizer powder materials. This article explores the fundamental principles behind such systems and highlights key application scenarios where their implementation proves beneficial.
The Core Principles of Air-Driven Transport
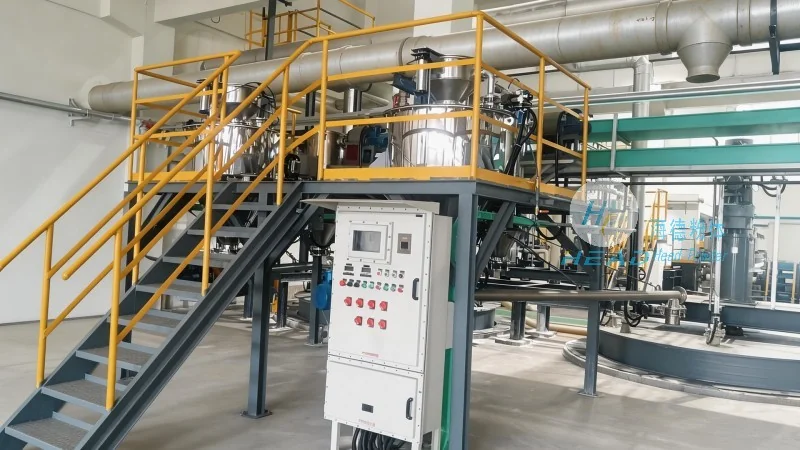
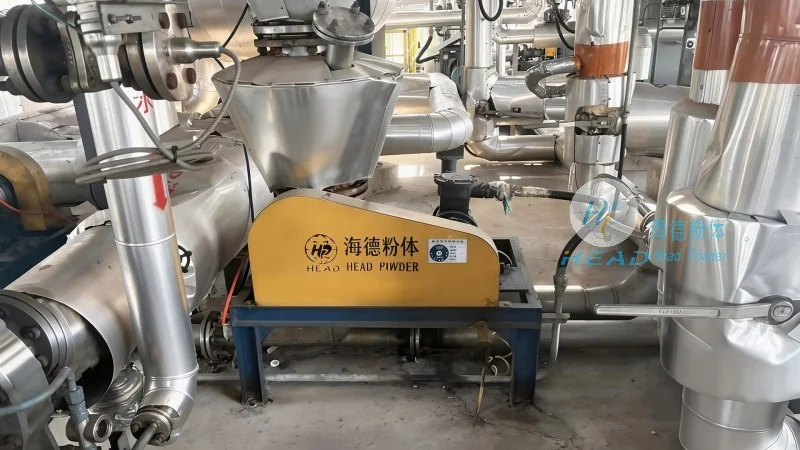
At the heart of air-driven transport systems lies the use of compressed air or other gas streams to move bulk materials through a network of pipes. For stabilizer powders, which often require precise control over flow rates and particle distribution, these systems offer a reliable alternative to traditional mechanical conveying methods. The process typically involves a hopper or feeder that introduces the powder into a duct, where a fan or blower generates the necessary airflow to propel the material. Key components include the feeding mechanism, the conveying line, and the discharge equipment, all working in tandem to ensure consistent and controlled material movement.
Key Technical Advantages of Air-Driven Transport
Compared to mechanical conveying, air-driven systems provide several advantages that are particularly valuable for stabilizer powders. These include reduced risk of material degradation due to minimal contact with equipment, enhanced flexibility in system layout as pipes can be easily reconfigured, and improved safety by eliminating the need for moving parts that could pose a hazard. Additionally, air-driven transport allows for precise control over particle velocity and distribution, which is crucial for maintaining the quality and consistency of stabilizer powders during handling and processing.
Common Application Scenarios
HeadPowder's air-driven transport solutions are widely applied in various industrial settings where stabilizer powders are processed. One primary scenario is in the chemical and pharmaceutical industries, where stabilizer powders are used as additives in manufacturing processes. Here, the systems ensure that the powders are delivered to reactors or mixing units with minimal segregation and contamination. Another common application is in the food and beverage sector, where stabilizers are used to enhance product texture and shelf life. The air-driven transport systems maintain the purity and quality of these powders, preventing cross-contamination and ensuring compliance with regulatory standards.
Industrial Processing and Manufacturing Environments
In industrial manufacturing, the efficiency of material handling directly impacts overall production throughput. Air-driven transport systems are integral to plants that produce stabilizer powders or use them as raw materials. For instance, in a fertilizer production facility, stabilizer powders are conveyed from storage silos to blending equipment using air-driven systems. This approach minimizes downtime and ensures a steady supply of materials, contributing to higher productivity. Similarly, in the production of personal care products, stabilizer powders are transported to mixing tanks, where they are combined with other ingredients. The controlled flow provided by air-driven systems helps maintain the desired consistency of the final product.
Customization and Scalability for Diverse Needs
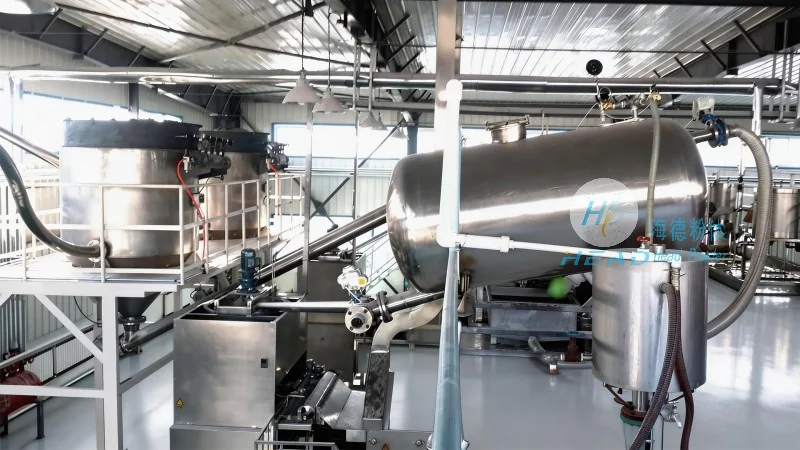
HeadPowder recognizes that each industrial application has unique requirements. Therefore, their air-driven transport systems are designed to be customizable and scalable. Clients can specify the type of fan, the diameter of the conveying line, and the control mechanisms to suit their specific needs. Whether handling small batches of stabilizer powders in a laboratory setting or large-scale production in a factory, the systems can be adjusted to meet the demands. This flexibility ensures that the transport solutions are not only efficient but also cost-effective, as they can be optimized for the specific volume and type of material being processed.
Conclusion and Company Overview
HeadPowder Engineering Co., Ltd., based in Shandong, China, has established itself as a trusted provider of air-driven transport solutions for stabilizer powder materials. By leveraging advanced technology and a deep understanding of industrial processes, the company offers systems that enhance efficiency, safety, and product quality. The principles and application scenarios discussed here underscore the importance of air-driven transport in modern industrial settings, and HeadPowder continues to innovate to meet the evolving needs of its clients.




