What is a Heavy Calcium Powder Conveying System? What are the Design Principles?
Release time:2026-09-14 14:29:17
name of the company:Shandong Headpowder Engineering Co., Ltd.
telephone:156-6277-7102
contacts:Zhang manager
Heavy calcium powder, also known as calcium carbonate, is a widely used industrial material in various sectors such as plastics, coatings, and paper. The efficient and reliable transportation of this powder is crucial for industrial processes. This article will explore the concept of a heavy calcium powder conveying system and delve into its fundamental design principles.
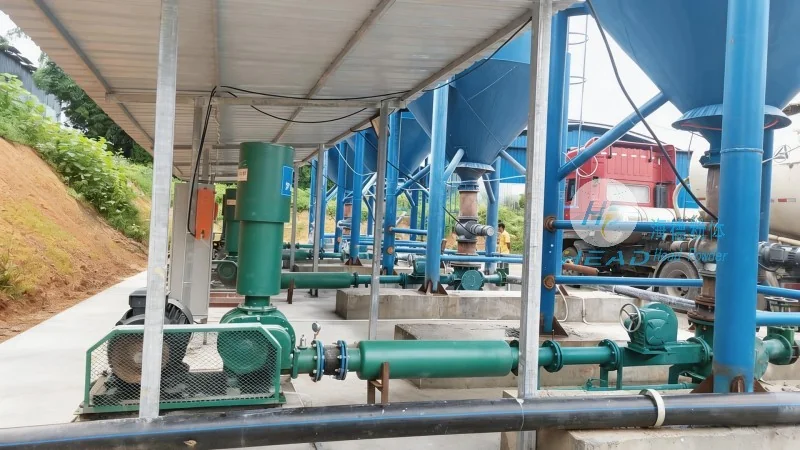
Understanding the Heavy Calcium Powder Conveying System
A heavy calcium powder conveying system is a specialized setup designed to transport calcium carbonate powder from its source to the processing or storage location. These systems are engineered to handle the unique characteristics of heavy calcium powder, which includes its high density, fine particle size, and potential for dust generation. The primary goal of such a system is to ensure smooth, continuous, and safe material flow while minimizing operational issues like blockages, material loss, or equipment wear.
Key Components of the Conveying System
The heavy calcium powder conveying system typically consists of several key components that work in tandem to achieve efficient material transport. These components include:
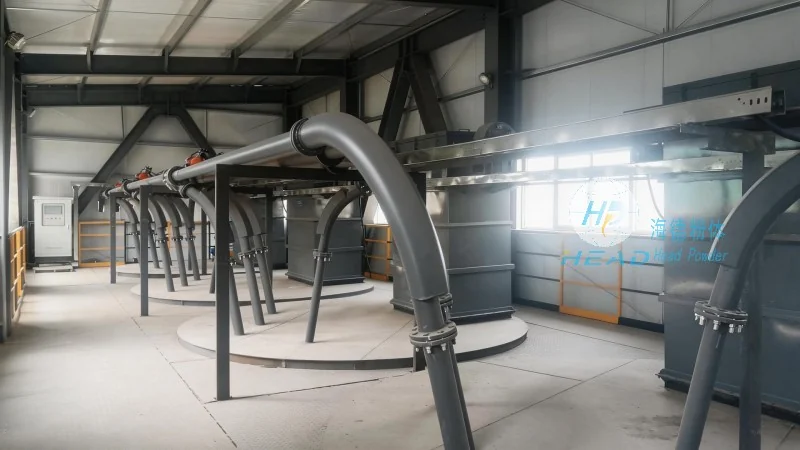
- Pneumatic Conveying Hoppers: These are the initial collection points where the heavy calcium powder is stored before being conveyed. They are designed to handle bulk quantities and ensure a consistent feed to the conveying line.
- Pneumatic Conveying Lines: The core of the system, these lines use air pressure to move the powder through a network of pipes. The design of these lines is critical as they must accommodate the high density and fine particle size of the powder without causing excessive pressure drops or blockages.
- Conveying Air Systems: This includes the blower or compressor that generates the necessary air pressure to move the powder. The air system must be capable of handling the specific flow rates and pressure requirements dictated by the powder characteristics and system design.
- Control and Monitoring Systems: Modern systems incorporate sensors and control units to monitor flow rates, pressure, and other critical parameters. This allows for real-time adjustments and ensures the system operates within optimal conditions.
Design Principles for Efficient Operation
The design of a heavy calcium powder conveying system is guided by several key principles to ensure efficiency, reliability, and safety. These principles include:
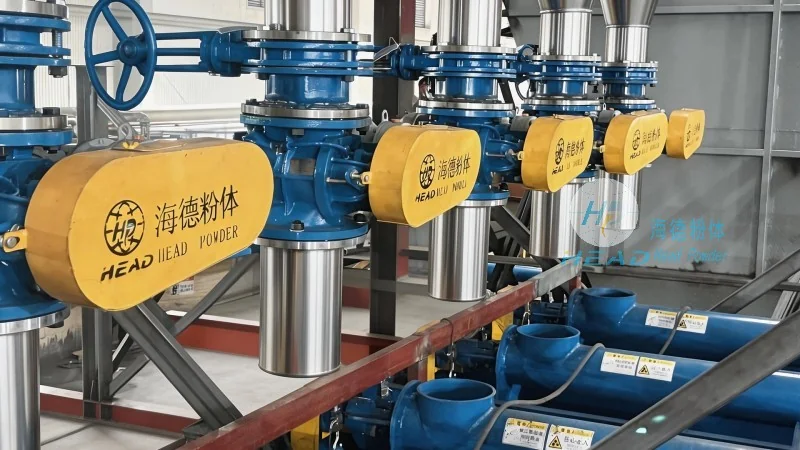
- Material Compatibility: All components of the system, including pipes, hoppers, and valves, must be compatible with calcium carbonate powder. This involves selecting materials that resist corrosion and abrasion, as the powder can be abrasive and may contain acidic components.
- System Sizing and Flow Rate: Proper sizing of the conveying lines and air systems is essential to maintain optimal flow rates. The design must account for the powder's density, particle size distribution, and the desired throughput to avoid excessive energy consumption or system strain.
- Prevention of Blockages: A critical design consideration is the prevention of blockages in the conveying lines. This is achieved through the use of appropriate pipe diameters, smooth internal surfaces, and the incorporation of cleaning mechanisms or anti-clogging features.
- Energy Efficiency: The system is designed to minimize energy consumption while maintaining performance. This includes optimizing air pressure, reducing pressure losses, and using efficient blower or compressor designs.
- Safety and Environmental Considerations: The design incorporates safety features to prevent dust explosions and ensure operator safety. Additionally, measures are taken to control dust emissions and maintain a clean working environment.
Applications and Benefits
Heavy calcium powder conveying systems are widely used in industries that rely on calcium carbonate as a raw material. The benefits of such systems include improved production efficiency, reduced labor costs, and enhanced safety in handling bulk materials. By ensuring a consistent and reliable supply of heavy calcium powder, these systems contribute to the overall productivity and quality of the end products.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of industrial conveying systems. With a focus on innovation and quality, HeadPowder specializes in designing and manufacturing heavy calcium powder conveying systems tailored to the specific needs of various industries. The company is headquartered in Shandong, China, and serves clients globally with its advanced technology and reliable products.




