Coal ash pneumatic conveying equipment is a key component in modern industrial processes, particularly in facilities that handle large volumes of coal ash. This equipment operates by using air pressure to transport coal ash from one location to another, offering an efficient and flexible solution for material handling. The core principle involves creating a pressure differential to move the material through a pipeline system, which can be either positive or negative pressure depending on the specific application requirements.
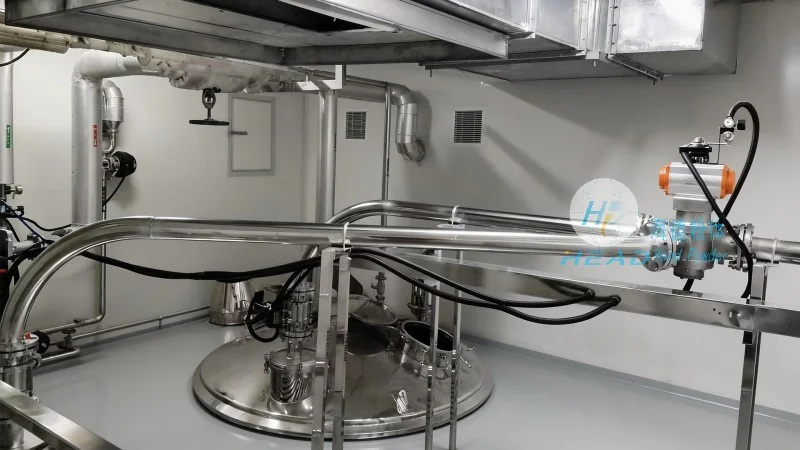
Working Principle of Coal Ash Pneumatic Conveying Systems
The operation of coal ash pneumatic conveying systems is based on the fundamental physics of fluid dynamics. The system typically consists of a hopper, a blower or fan, a pipeline network, and a receiver. When the system is activated, the blower generates a flow of air that draws the coal ash from the hopper into the pipeline. The air velocity is maintained at a level sufficient to keep the ash particles suspended, preventing them from settling or clogging the pipeline. This process ensures a continuous and reliable flow of material, minimizing downtime and maintenance costs.
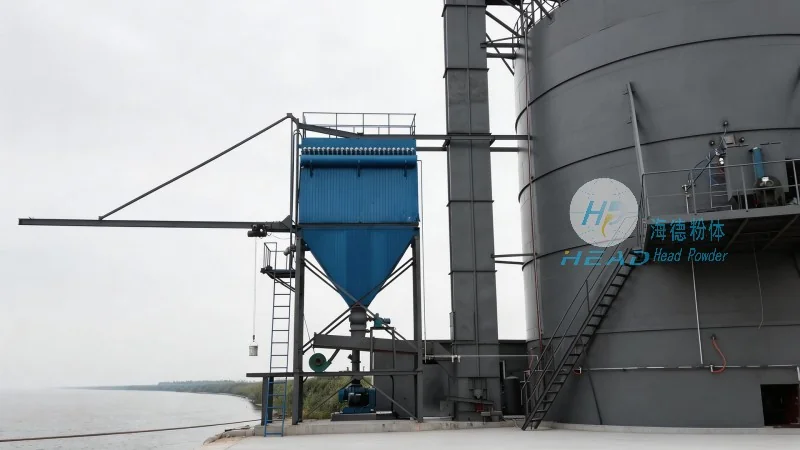
Key Working Scene Characteristics
Coal ash pneumatic conveying equipment is widely used in various industrial settings due to its adaptability and efficiency. One of the primary characteristics is its ability to handle abrasive and fine materials like coal ash, which are prone to wear and tear in traditional conveyor systems. The equipment's design allows for long-distance transportation with minimal loss of material, making it suitable for applications where material is transported over several hundred meters or more. Additionally, the system can be integrated with other industrial processes, such as drying or mixing, to create a comprehensive material handling solution.
Application Scenarios and Industry Use Cases
In power plants, coal ash pneumatic conveying systems are crucial for transporting ash from the boiler to storage or disposal sites. The equipment can handle the high volume of ash produced by modern power generation facilities, ensuring that the material is moved safely and efficiently. In cement plants, the system is used to transport raw materials like limestone and coal ash, which are essential for the production of cement. The flexibility of the pneumatic conveying system allows for adjustments in material flow rates, accommodating varying production demands. Furthermore, in recycling facilities, the equipment can be used to transport recycled materials, contributing to sustainable industrial practices.
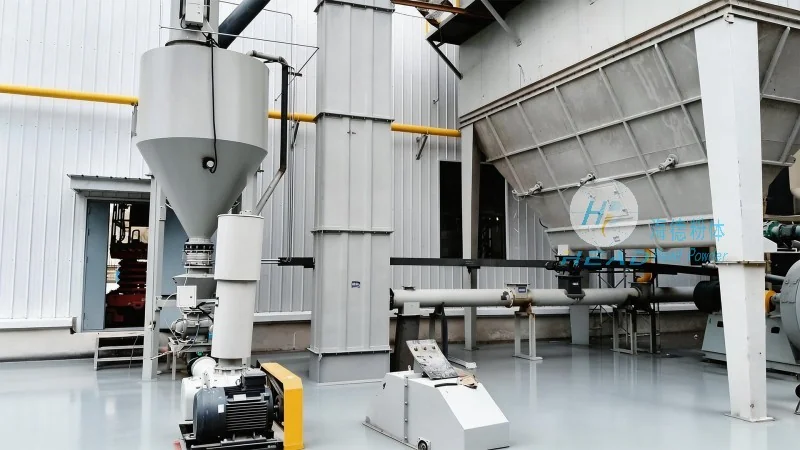
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading manufacturer of coal ash pneumatic conveying equipment. With a strong focus on innovation and quality, the company has established itself as a trusted partner in the industrial material handling sector. HeadPowder's products are designed to meet the specific needs of various industries, offering reliable and efficient solutions for coal ash transportation. The company's headquarters is located in Shandong, China, where it has a dedicated team of engineers and technicians dedicated to research, development, and customer support.




