For industrial applications requiring efficient and reliable material handling, the bulk material mixing pneumatic conveying machine stands out as a versatile solution. This equipment is designed to transport and blend various dry powders and granules in a controlled environment, ensuring consistent product quality and operational efficiency. The core of its functionality lies in the pneumatic conveying system, which utilizes air pressure to move materials through a network of pipes and components. Manufactured by Shandong HeadPowder Engineering Co., Ltd., a leading provider of industrial material handling solutions based in Shandong, China, this equipment exemplifies advanced pneumatic conveying technology.
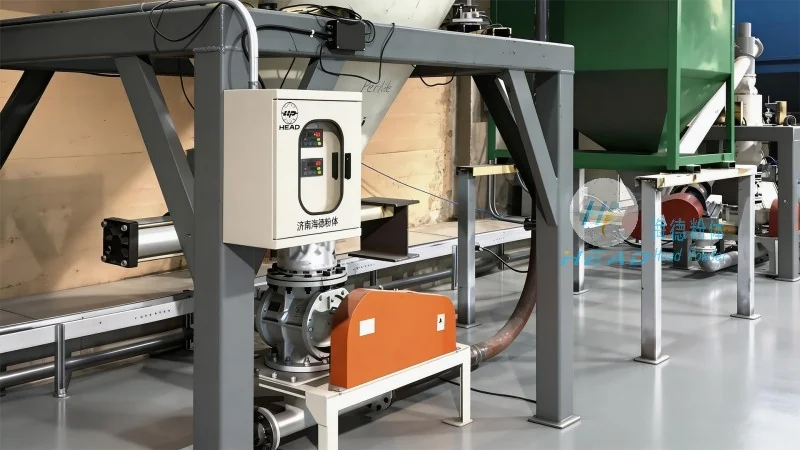
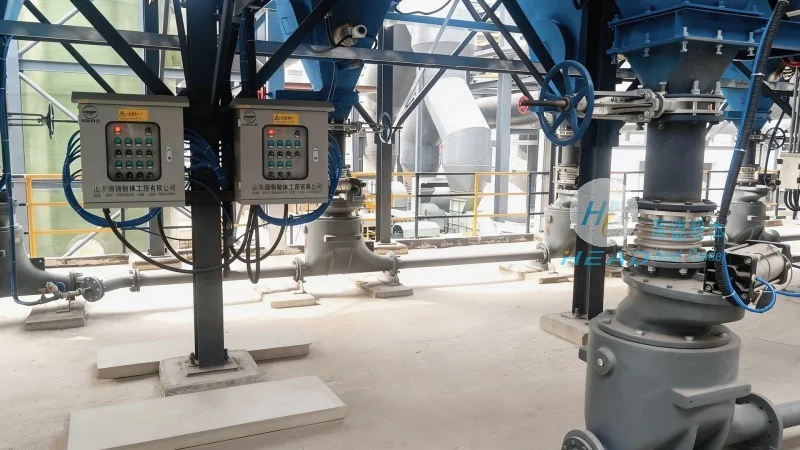
Working Principle of the Bulk Material Mixing Pneumatic Conveyor
The operation of a bulk material mixing pneumatic conveyor is based on the principles of fluid dynamics and material flow. Typically, the system operates under either positive pressure (pressure conveying) or negative pressure (suction conveying). In positive pressure systems, compressed air is introduced into the material hopper, creating a pressure differential that propels the material through the pipeline. The air and material mixture then travels to the destination point, where the material is separated from the air using a cyclone separator or other filtration equipment. For negative pressure systems, a vacuum is created at the discharge end, drawing the material from the source into the pipeline. The mixing process is achieved by strategically placing mixing zones within the pipeline, where the material is agitated and combined with other ingredients as it moves through the system. This ensures that the final product has a uniform composition, which is critical for applications such as pharmaceuticals, food processing, and chemical manufacturing.
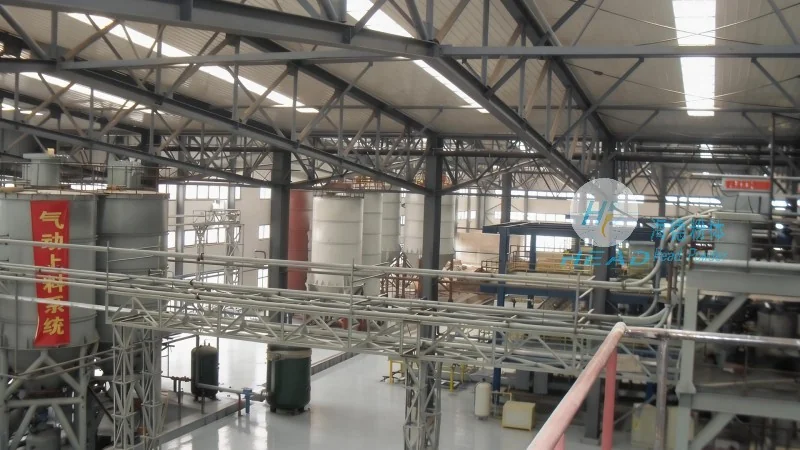
Key Working Scene Characteristics
The bulk material mixing pneumatic conveyor is particularly suited for environments where dust control, hygiene, and precise material control are paramount. Its enclosed system prevents material contamination and minimizes the risk of dust exposure, making it ideal for industries where product purity is a top priority. Additionally, the system's ability to handle a wide range of materials—from fine powders to coarse granules—provides flexibility in production processes. The mixing capability allows for the combination of multiple ingredients in real-time, reducing the need for separate blending steps and streamlining the overall production workflow. This leads to increased productivity and cost savings for manufacturers. The equipment is also designed for easy integration into existing production lines, with modular components that can be customized to meet specific operational requirements. This adaptability makes it a preferred choice for both new installations and retrofits in various industrial settings.
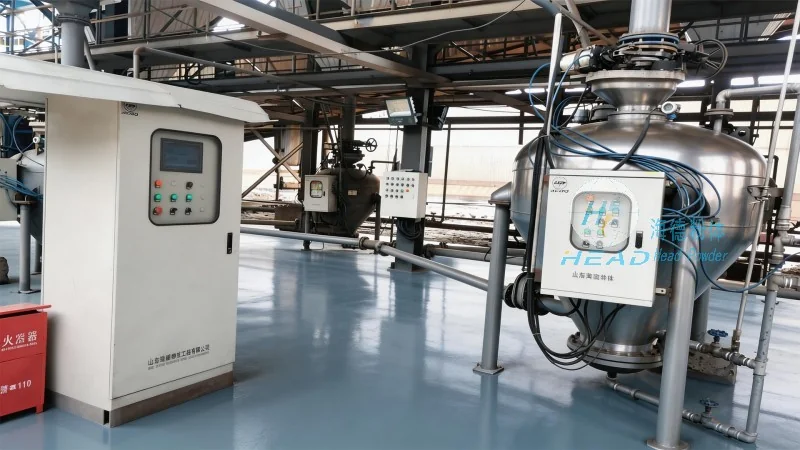
Application Examples and Operational Benefits
In practical applications, the bulk material mixing pneumatic conveyor is commonly used in the pharmaceutical industry for the transport and mixing of active pharmaceutical ingredients (APIs) and excipients. The enclosed system ensures that these materials remain sterile and free from contamination, which is essential for meeting regulatory standards. In the food processing sector, it is employed to handle ingredients like flour, sugar, and spices, maintaining product freshness and preventing cross-contamination. The chemical industry also benefits from this technology when handling powders such as pigments, catalysts, and reagents, where precise mixing and dust control are critical. The operational benefits of this equipment include reduced labor costs due to automated material handling, lower energy consumption compared to traditional mechanical conveyors, and improved safety by eliminating manual handling of powders. Furthermore, the system's compact design allows for space-efficient installations, making it suitable for facilities with limited floor space. Overall, the bulk material mixing pneumatic conveyor offers a comprehensive solution for material handling and blending, enhancing operational efficiency and product quality across diverse industrial applications.




