Automatic bulk powder unpacking and pneumatic conveying equipment is a specialized system designed to handle the efficient and safe transfer of bulk powders from storage containers to processing lines. This equipment integrates advanced technologies to streamline the entire material handling process, ensuring minimal human intervention and maximizing operational efficiency. The system is particularly valuable in industries such as pharmaceuticals, food processing, chemical manufacturing, and other sectors where precision and hygiene are critical.
Principle of Operation
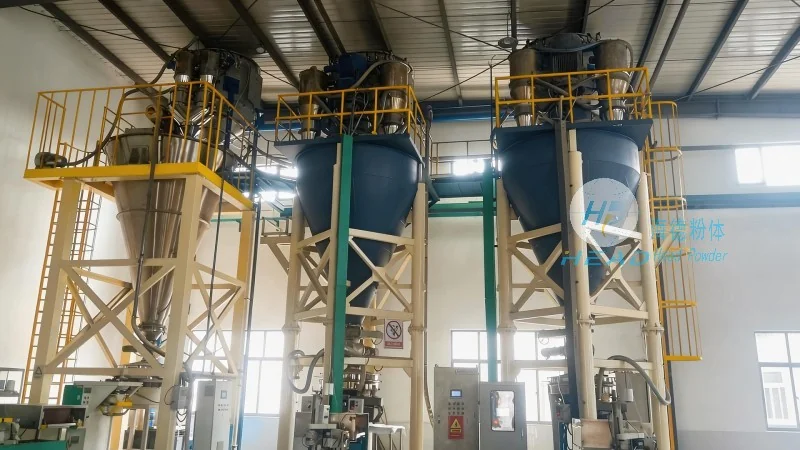
The core principle of this equipment lies in the combination of automated unpacking mechanisms and pneumatic conveying technology. The process begins with the detection and opening of bulk powder bags or containers, followed by the controlled discharge of the powder into a hopper or feeder. From there, the material is transported through a network of pipes using compressed air or other gas streams, creating a pressure differential that propels the powder forward. The system typically includes components like rotary valves, cyclone separators, and dust collectors to ensure the material is conveyed without degradation and the environment remains clean and safe.
Working Scene Characteristics
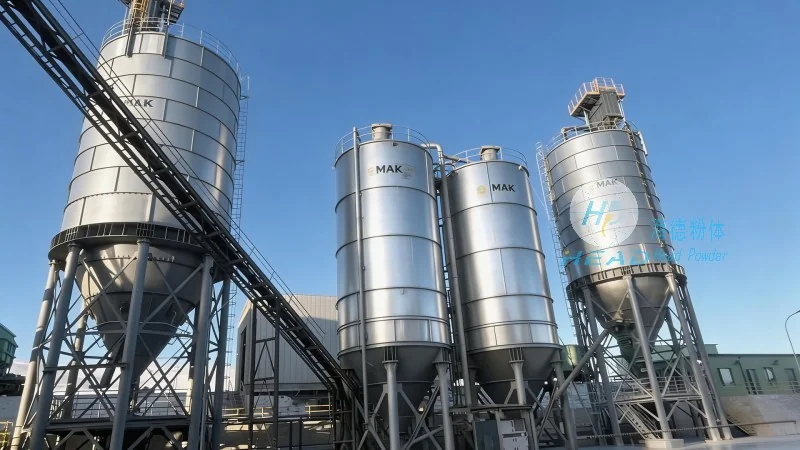
The application scenarios for this equipment vary widely based on the industry and the specific requirements of the production line. In pharmaceutical manufacturing, for instance, the equipment operates under strict GMP (Good Manufacturing Practice) guidelines, ensuring that powders are handled in a sterile and controlled environment. The automated nature of the system minimizes cross-contamination risks and maintains consistent product quality. In the food industry, similar standards apply, with the equipment designed to handle food-grade powders while adhering to hygiene and safety regulations. Chemical manufacturers benefit from the ability to handle a wide range of powders, from fine chemicals to bulk raw materials, with the system's adaptability allowing for different particle sizes and flow characteristics. Additionally, the equipment is suitable for applications in research and development labs, where precise dosing and minimal waste are essential.
Key Features and Advantages
One of the primary advantages of this equipment is its ability to reduce labor costs and improve operational safety. By automating the unpacking and conveying process, the system eliminates the need for manual handling of heavy or hazardous powders, reducing the risk of workplace injuries and exposure to harmful substances. The integration of dust collection systems ensures that the air quality in the facility remains within safe limits, complying with environmental regulations. Another key feature is the system's flexibility, which allows it to handle various types of containers, including bags, big bags, and drums, with minimal adjustments. The modular design of the equipment enables easy integration into existing production lines, and its low maintenance requirements contribute to long-term cost savings.
About Shandong HeadPowder Engineering Co., Ltd.
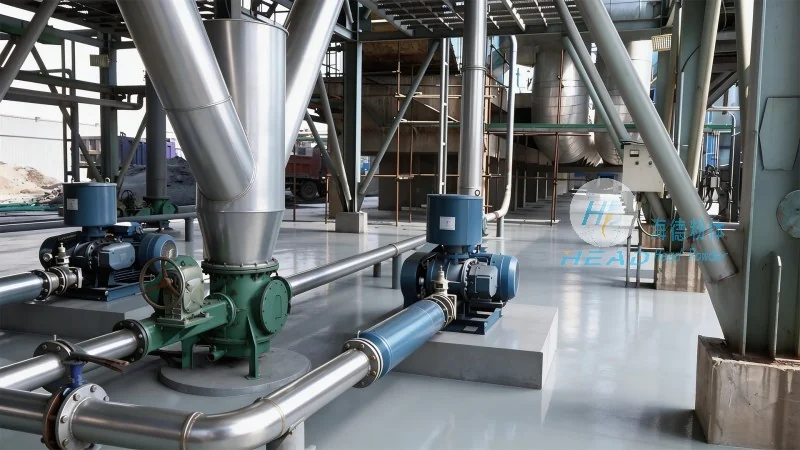
HeadPowder, a leading manufacturer in the field of bulk material handling solutions, specializes in the design, development, and production of advanced automatic powder unpacking and pneumatic conveying equipment. With a strong commitment to innovation and quality, the company has established itself as a trusted partner for industries worldwide. HeadPowder's products are engineered to meet the highest standards of performance, reliability, and safety, ensuring that customers receive equipment that is tailored to their specific needs. The company's headquarters is located in Shandong, China, where a team of experienced engineers and technicians work tirelessly to deliver cutting-edge solutions that enhance operational efficiency and product quality.




