For clients seeking efficient and reliable methods to handle potassium carbonate fertilizer, the pneumatic conveying system offers a sophisticated solution. This technology is integral to modern fertilizer processing and distribution, ensuring that the material is transported safely and effectively from storage to processing or packaging units. The following sections detail the operational process and underlying principles of this system, highlighting its benefits and the expertise of Shandong HeadPowder Engineering Co., Ltd. in implementing such solutions.
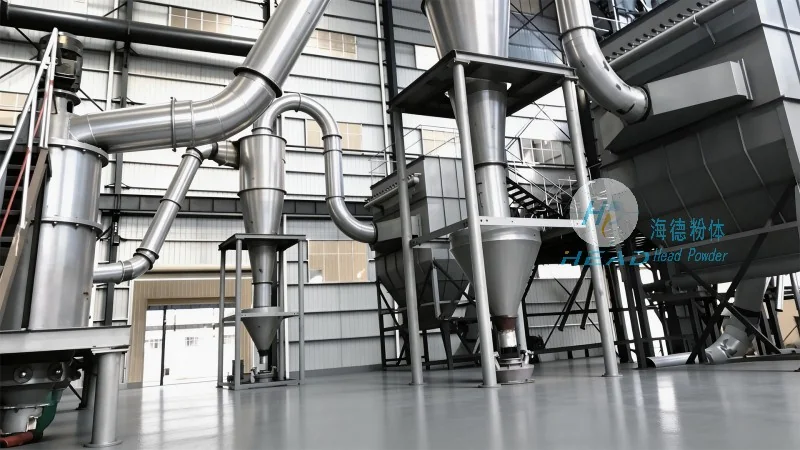
Introduction to Pneumatic Conveying for Potassium Carbonate Fertilizer
Potassium carbonate, a vital component in agricultural fertilizers, requires specialized handling due to its granular or powdery nature. Traditional methods like belt conveyors or bucket elevators may not be suitable for fine or dusty materials, as they can lead to material degradation, increased wear, or environmental issues. Pneumatic conveying systems provide a dust-free, enclosed solution that minimizes product loss and contamination. Shandong HeadPowder Engineering Co., Ltd., a leading provider in the field, specializes in designing and manufacturing custom pneumatic conveying systems tailored to the unique characteristics of potassium carbonate fertilizer.
The Core Components of a Pneumatic Conveying System
A pneumatic conveying system for potassium carbonate fertilizer typically consists of several key components that work in tandem to achieve efficient material transport. These include the hopper or feed bin, the air mover (such as a rotary lobe blower or positive displacement blower), the conveying line (often made of stainless steel to prevent corrosion from the fertilizer), and the receiver or discharge hopper. Each component plays a critical role in the overall operation, ensuring that the fertilizer is moved with minimal disruption and maximum efficiency.
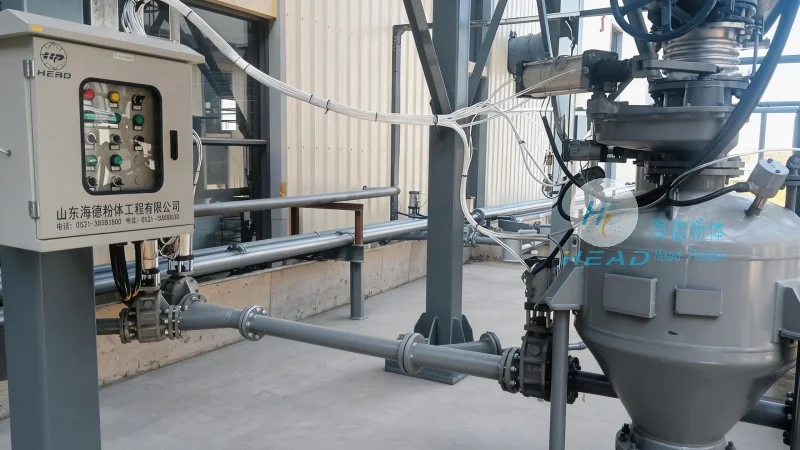
Step-by-Step Operation Process
The operation of a pneumatic conveying system for potassium carbonate fertilizer involves a sequence of actions that ensure smooth and continuous material flow. The process begins with the material being fed from the storage hopper into the conveying line. The air mover then generates a high-pressure airflow that pulls the fertilizer particles into the line. As the material travels through the pipeline, it is suspended and transported to the receiving hopper at the destination. The system may include additional components such as filters to capture any fine particles and prevent them from escaping into the environment, ensuring compliance with environmental regulations.
Working Principle: Airflow and Particle Suspension
The fundamental principle behind pneumatic conveying is the use of air to suspend and transport solid particles. In the case of potassium carbonate fertilizer, the air mover creates a pressure differential that draws the material into the conveying line. The velocity of the air is crucial; it must be sufficient to lift and carry the particles without causing excessive wear on the system components. The system's design, including the diameter and length of the pipeline, the type of air mover, and the feed mechanism, all contribute to optimizing the airflow and particle suspension. Shandong HeadPowder Engineering Co., Ltd. employs advanced engineering techniques to ensure that the system operates at the optimal airflow rates, minimizing energy consumption while maximizing conveying efficiency.
Advantages of Pneumatic Conveying for Potassium Carbonate Fertilizer
Implementing a pneumatic conveying system for potassium carbonate fertilizer offers several advantages over traditional methods. Firstly, it provides a dust-free environment, reducing the risk of inhalation hazards and minimizing product loss due to dust. Secondly, the enclosed system prevents contamination from external sources, maintaining the purity of the fertilizer. Thirdly, the system is highly flexible, allowing for changes in the conveying route or capacity without major modifications. Additionally, the use of stainless steel components ensures durability and resistance to corrosion from the alkaline nature of potassium carbonate. Shandong HeadPowder Engineering Co., Ltd. leverages these advantages to deliver systems that enhance operational efficiency and product quality for their clients.
Customization and Application in Fertilizer Processing
Every fertilizer processing facility has unique requirements, and Shandong HeadPowder Engineering Co., Ltd. recognizes the importance of customization. The company works closely with clients to understand their specific needs, such as the volume of fertilizer to be conveyed, the distance between the feed and discharge points, and any environmental or safety regulations that must be adhered to. Based on this information, they design a tailored pneumatic conveying system that meets all operational and regulatory standards. The systems are typically integrated into existing processing lines, ensuring a seamless transition and minimal disruption to production. Whether for small-scale operations or large industrial facilities, the company's expertise in pneumatic conveying ensures that clients receive a solution that is both effective and cost-efficient.
Conclusion and Company Expertise
Pneumatic conveying is a critical technology for the efficient handling of potassium carbonate fertilizer, and Shandong HeadPowder Engineering Co., Ltd. stands as a trusted partner in implementing these systems. By understanding the unique properties of the fertilizer and the operational needs of their clients, the company designs, manufactures, and installs custom pneumatic conveying solutions that enhance productivity, safety, and environmental compliance. With a focus on quality and customer satisfaction, Shandong HeadPowder Engineering Co., Ltd. continues to provide reliable and innovative solutions for the fertilizer industry, ensuring that clients can meet their production goals while maintaining the highest standards of product quality and safety.




