Fertilizer pneumatic conveying systems are critical components in modern agricultural and industrial operations, designed to efficiently transport bulk fertilizers from storage facilities to application points. These systems leverage the principles of air movement to move granular or powdered materials, offering a reliable and cost-effective solution for handling large volumes of fertilizer. The operation and working principles of such systems are essential for understanding their efficiency, maintenance, and application in various settings.
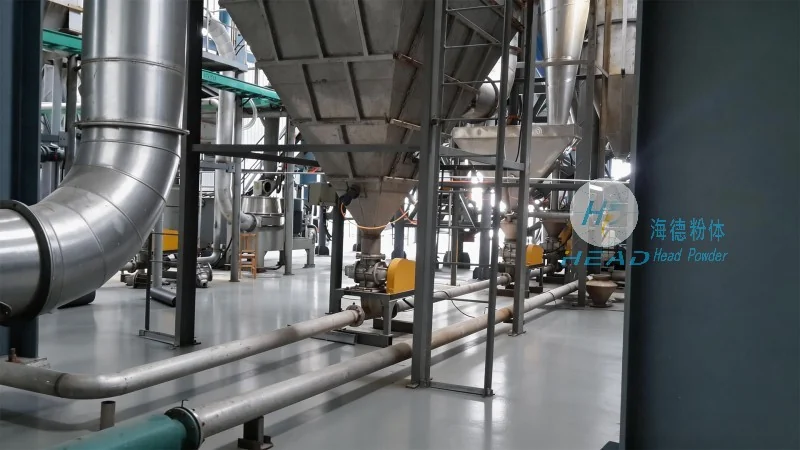
Key Components of a Fertilizer Pneumatic Conveying System
At the core of a fertilizer pneumatic conveying system are several key components that work in tandem to ensure smooth material transport. These include the hopper or storage bin, which holds the fertilizer; the air mover (such as a blower or fan) that generates the necessary airflow; the pipeline system that carries both the material and air; and the control valves and sensors that regulate the flow and pressure. Each component plays a vital role in maintaining the system's performance and preventing issues like blockages or excessive pressure.
The Operation Process of Fertilizer Pneumatic Conveying
The operation process of a fertilizer pneumatic conveying system typically begins with the material being fed from the storage hopper into the system. The air mover then activates, creating a flow of air through the pipeline. As the air moves, it entrains the fertilizer particles, lifting them along the pipeline to the destination point. The system may use different conveying modes, such as dilute phase or dense phase, depending on the material characteristics and distance to be covered. Dilute phase systems are suitable for shorter distances and lighter materials, while dense phase systems are used for longer distances or bulkier materials, as they maintain a higher material concentration in the air stream.
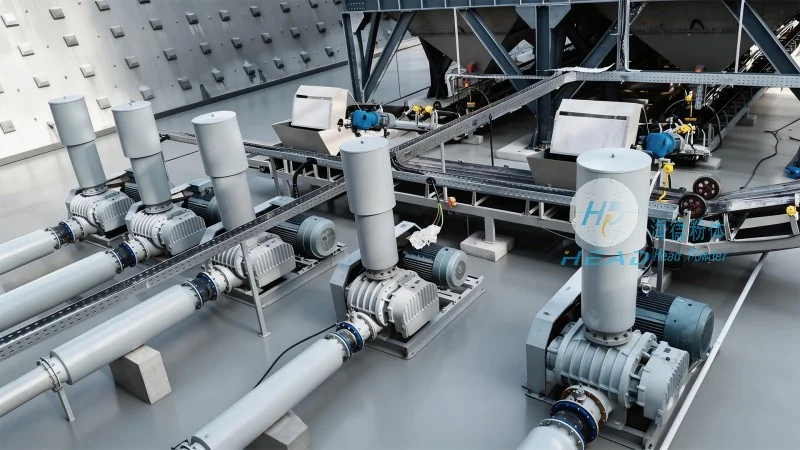
Working Principle of Fertilizer Pneumatic Conveying
The working principle of a fertilizer pneumatic conveying system is based on the interaction between air and the fertilizer particles. When the air mover operates, it generates a pressure difference between the inlet and outlet of the system. This pressure difference creates a flow of air that carries the fertilizer particles through the pipeline. The velocity of the air is crucial; it must be sufficient to lift and transport the particles without causing excessive wear on the system components. The system may also incorporate features like cyclones or separators at the receiving end to separate the fertilizer from the air, ensuring that the material is deposited accurately and the air is filtered before release.
Advantages of Using Fertilizer Pneumatic Conveying Systems
Implementing a fertilizer pneumatic conveying system offers several advantages over traditional methods like truck or belt conveyors. These systems are highly efficient in terms of energy consumption, as they use air to move the material rather than mechanical components. They also reduce labor costs and the risk of material spillage or contamination, as the entire process is enclosed and controlled. Additionally, pneumatic conveying systems can handle a wide range of fertilizer types, from granular to powdered, and can be easily integrated into existing agricultural or industrial facilities. The ability to transport materials over long distances without the need for intermediate storage points also enhances operational flexibility and reduces downtime.
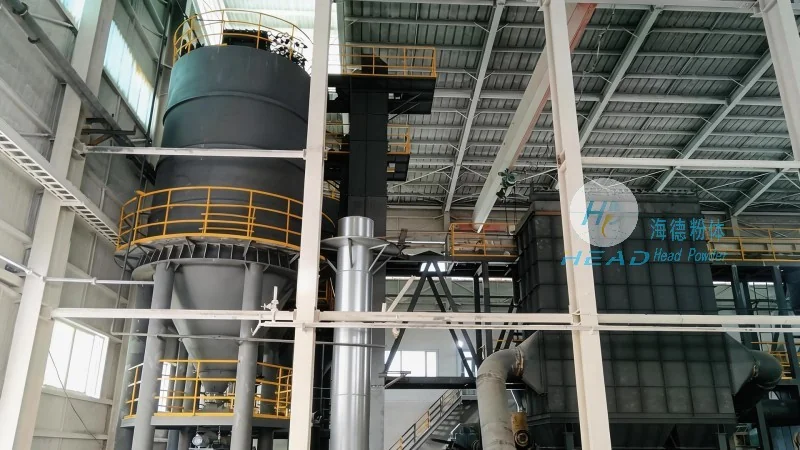
Maintenance and Best Practices for Fertilizer Pneumatic Conveying Systems
To ensure the longevity and optimal performance of a fertilizer pneumatic conveying system, regular maintenance is essential. This includes checking the air mover for proper operation, inspecting the pipeline for blockages or leaks, and cleaning the cyclones or filters at the receiving end. It is also important to monitor the system's pressure and flow rates to detect any deviations that may indicate a problem. Proper training for operators on the system's operation and maintenance can prevent common issues and extend the system's lifespan. Additionally, using high-quality materials for the pipeline and components can reduce wear and tear, ensuring consistent performance over time.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading manufacturer and supplier of fertilizer pneumatic conveying systems. With a focus on innovation and quality, the company has developed advanced systems that meet the diverse needs of agricultural and industrial clients. Headpowder's products are designed to be efficient, reliable, and easy to maintain, ensuring that clients can achieve optimal performance in their fertilizer handling operations. The company's commitment to customer satisfaction and technical excellence has made it a trusted partner in the industry, providing solutions that enhance productivity and reduce operational costs.




