At Shandong HeadPowder Engineering Co., Ltd., we specialize in the design, manufacturing, and implementation of advanced fine powder pneumatic conveying systems. These systems are crucial for efficiently transporting fine powders over varying distances, ensuring minimal product degradation and maintaining high operational efficiency. The technology is widely used across industries such as pharmaceuticals, chemicals, food processing, and mining, where handling fine powders requires precision and reliability.
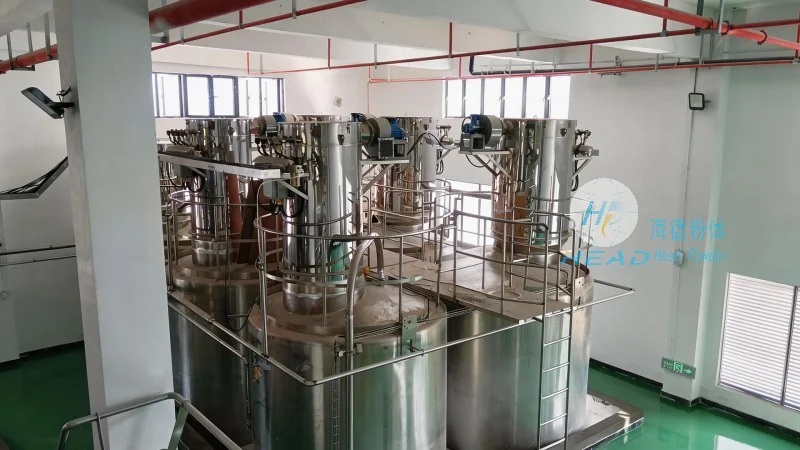
Key Components and Working Principle
A fine powder pneumatic conveying system typically consists of several core components that work in tandem to achieve effective material transport. The primary components include a feeding device, a conveying pipeline, a blower or compressor, a separation unit, and a discharge system. The working principle revolves around the use of air or gas to create a flow that propels the fine powder particles through the pipeline. The system operates by drawing the powder into the pipeline using the air flow, which is then directed to the destination point for collection or further processing.
Step-by-Step Operation Process
The operation of a fine powder pneumatic conveying system involves a series of controlled steps to ensure smooth and efficient material transport. The process begins with the feeding stage, where the fine powder is introduced into the system, often via a hopper or a rotary valve. This stage is critical as it ensures a consistent flow of material into the pipeline, preventing blockages or uneven distribution. Next, the conveying stage begins, where the blower or compressor generates the necessary air pressure to move the powder through the pipeline. The air flow is carefully regulated to maintain the optimal velocity for the powder particles, which helps in preventing particle agglomeration and ensuring uniform transport. During this stage, the powder is suspended in the air stream, traveling through the pipeline to the receiving end.
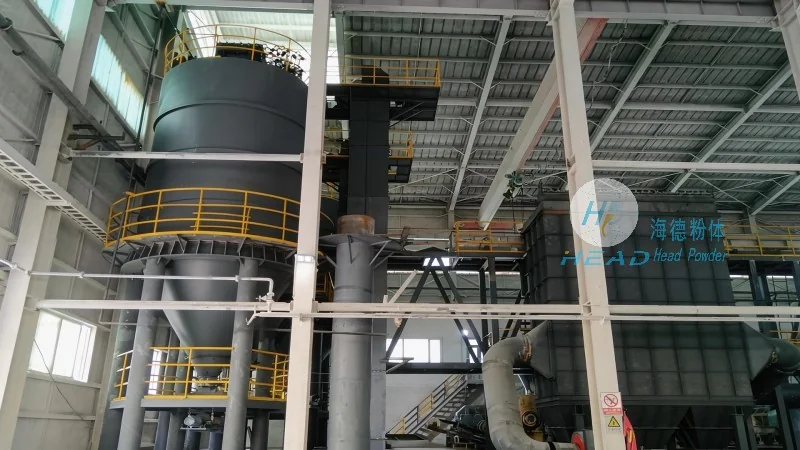
Following the conveying stage is the separation stage, where the powder is separated from the air stream and collected. This is typically achieved using a cyclone separator or a bag filter, which utilizes centrifugal force to separate the heavier powder particles from the lighter air. The separated powder is then directed to a discharge hopper or storage tank, while the clean air is either vented to the atmosphere or recirculated back into the system to enhance energy efficiency. The final stage involves the discharge and storage, where the collected powder is transferred to its intended destination, such as a processing unit or a storage silo. This stage ensures that the material is handled safely and efficiently, minimizing the risk of dust emissions and product contamination.
Advantages and Applications
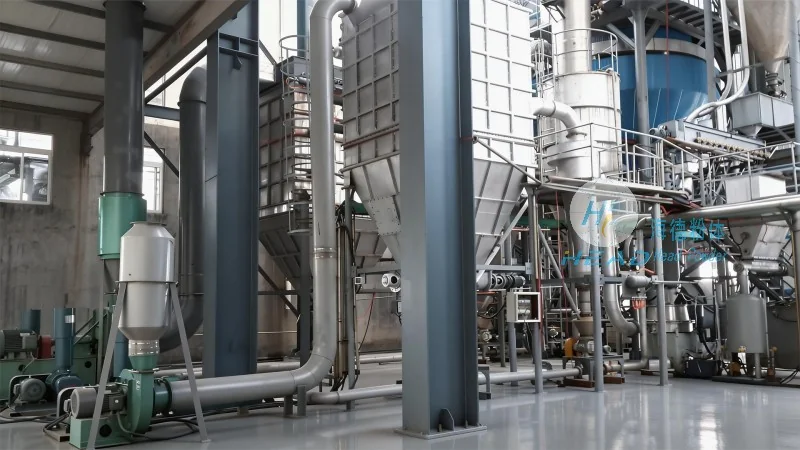
Fine powder pneumatic conveying systems offer several advantages over traditional mechanical conveying methods. These include reduced product degradation due to minimal contact with equipment, lower maintenance costs as there are fewer moving parts, and improved safety by minimizing dust exposure. The systems are also highly flexible, allowing for easy integration into existing production lines and adaptation to varying material characteristics. In the pharmaceutical industry, for example, these systems are used to transport active pharmaceutical ingredients (APIs) with high precision, ensuring compliance with stringent quality standards. In the chemical industry, they are employed to handle hazardous powders, providing a safe and controlled environment for material transport. The versatility of fine powder pneumatic conveying systems makes them suitable for a wide range of applications, from small-scale laboratory operations to large-scale industrial production.
Company Expertise and Commitment
Shandong HeadPowder Engineering Co., Ltd. is committed to delivering high-quality fine powder pneumatic conveying systems that meet the specific needs of our clients. With years of experience in the field, our team of engineers and technicians specializes in designing customized solutions that optimize material transport efficiency while ensuring compliance with industry standards and regulations. We provide comprehensive services, including system design, installation, commissioning, and after-sales support, to ensure that our clients achieve maximum operational performance and reliability. Our company is located in Shandong, China, and we pride ourselves on our ability to deliver innovative and efficient solutions tailored to the unique requirements of each project.




