HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and manufacturing of advanced pneumatic conveying systems tailored for handling bulk materials like coke and limestone powder. This article delves into the fundamental principles of such equipment and highlights the key characteristics of its operational environments.
Introduction to Pneumatic Conveying Systems for Bulk Materials
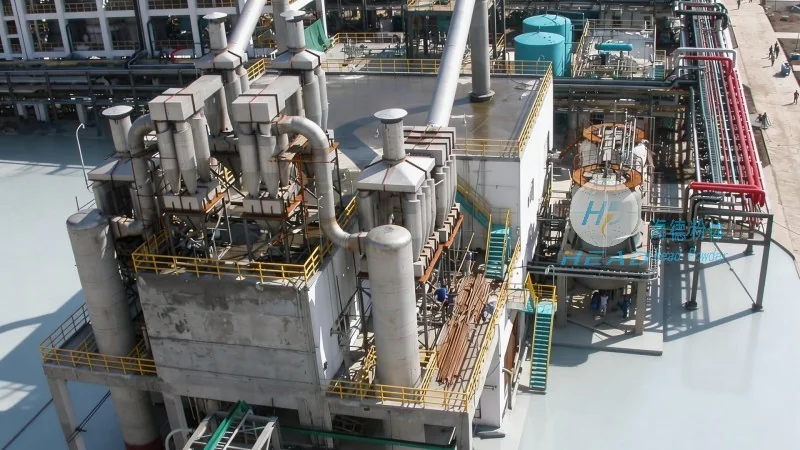
At the core of material handling in industrial settings, pneumatic conveyors offer an efficient and flexible solution for transporting fine powders and granular materials. The system operates by using compressed air or gas to move the material through a pipeline network, eliminating the need for mechanical components like belts or buckets. This method is particularly advantageous for materials that are prone to dust, require dust control, or need to be transported over long distances without degradation.
Principle of Operation for Coke and Limestone Powder Pneumatic Conveyors
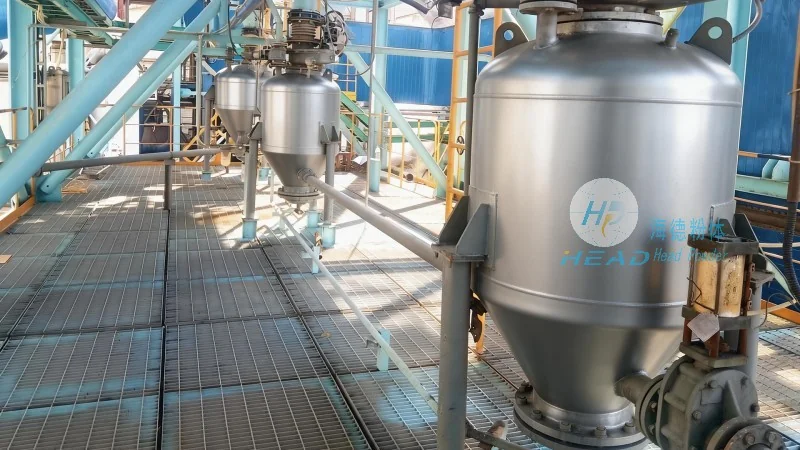
The operation of a pneumatic conveyor for coke and limestone powder involves several critical steps. First, the material is fed into a hopper or feeder, where it is then introduced into the conveying line. Compressed air, typically supplied by a blower or compressor, is introduced at the inlet of the pipeline. As the air flows through the line, it creates a pressure differential that propels the material forward. The design of the system, including the size of the pipeline, the velocity of the air, and the angle of the line, is crucial for ensuring efficient and consistent transport. The system may include features such as cyclone separators or filters to capture any dust or particles that may escape, maintaining air quality and preventing material loss.
Key Working Scene Characteristics
The effectiveness of a pneumatic conveyor for coke and limestone powder is heavily influenced by the operational environment. Several factors define these characteristics:
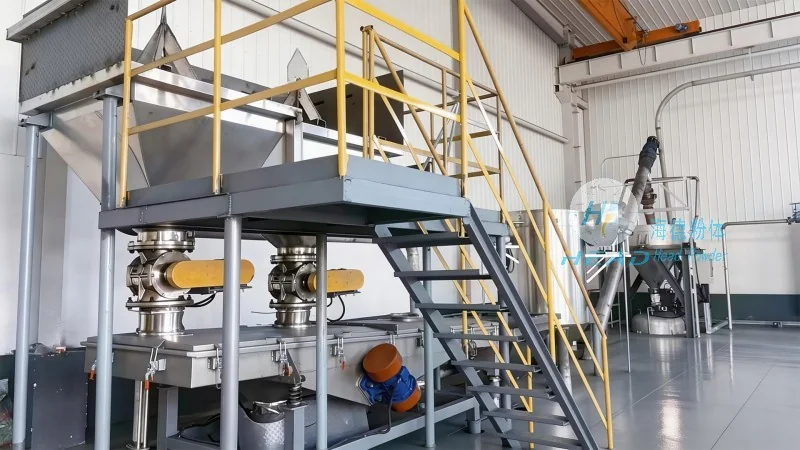
- Material Properties: The physical characteristics of coke and limestone powder, including particle size, density, and moisture content, directly impact the conveying efficiency. Coarser particles may require higher air velocities to maintain flow, while finer powders can be more susceptible to clogging or dust generation.
- Transport Distance and Layout: The length and configuration of the conveying line are critical. Longer distances may necessitate multiple stages of conveying, such as a combination of dilute-phase and dense-phase systems, to maintain material velocity and prevent settling. The layout of the plant, including the position of the feeder, discharge point, and any intermediate storage or processing units, must be carefully planned to optimize the system's performance.
- Dust Control and Environmental Considerations: Given that coke and limestone are often dusty materials, the system must incorporate robust dust control measures. This includes the use of sealed hoppers, cyclone separators, and filtration systems to minimize airborne particulates. Compliance with environmental regulations regarding air quality is essential, making the design of the conveying system a key consideration for industrial applications.
- System Integration and Automation: Modern pneumatic conveying systems are often integrated with other plant processes, such as storage silos, processing units, or packaging lines. Automation plays a vital role in controlling the flow rate, pressure, and timing of material transport, ensuring seamless operation and reducing the need for manual intervention. The ability to integrate with existing infrastructure while maintaining efficiency is a significant advantage of these systems.
Applications and Benefits in Industrial Settings
Pneumatic conveyors for coke and limestone powder find widespread application in various industrial sectors. In the steel industry, for example, coke is a critical raw material used in blast furnaces, and efficient transport is essential for maintaining production schedules. Similarly, in cement and mineral processing industries, limestone is a primary ingredient, and the ability to handle it in a dust-free manner enhances product quality and operational safety. The benefits of using such systems include reduced labor costs, improved material handling efficiency, minimized material loss, and enhanced workplace safety due to the enclosed nature of the conveying process.
Conclusion
Understanding the principle of operation and the working scene characteristics of a pneumatic conveyor for coke and limestone powder is essential for selecting and implementing an effective material handling solution. HeadPowder, with its expertise in engineering and manufacturing, provides tailored solutions that address the specific needs of industrial applications. By focusing on material properties, system design, and operational efficiency, these conveyors offer a reliable and sustainable method for transporting bulk materials in various industrial environments.




