HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced pneumatic conveying systems tailored for the transportation of cement and mineral powders. These systems are essential in modern industrial applications, offering efficient, dust-free, and reliable solutions for material handling. The following content explores the fundamental principles of such equipment and highlights key working scene characteristics that make them ideal for various industrial environments.
The Principle of Pneumatic Conveying for Cement and Mineral Powders
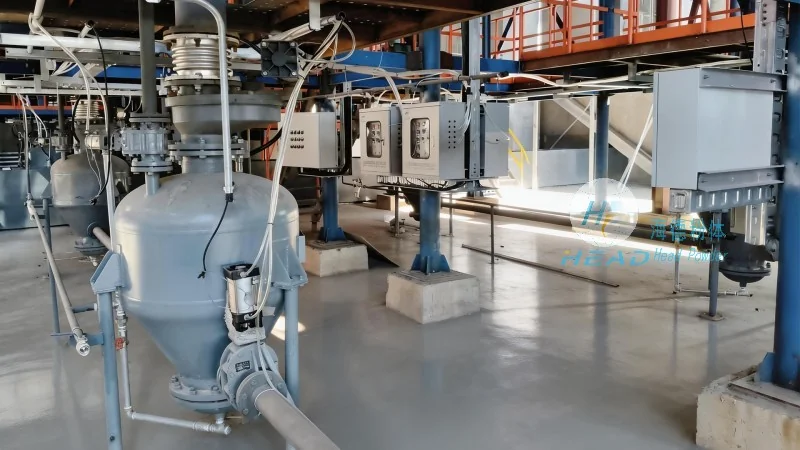
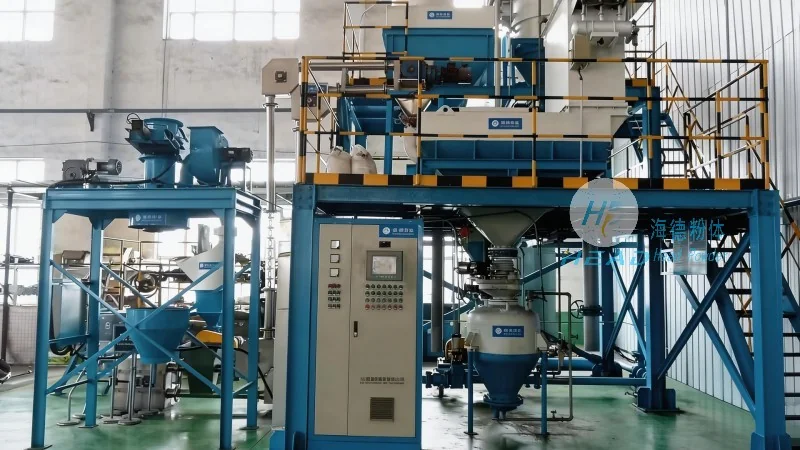
The core principle of cement and mineral powder pneumatic conveying involves the use of air as the medium to transport bulk materials. The system typically consists of a feeding hopper, a conveying pipeline, a pressure or vacuum source, and a discharge unit. When the material is introduced into the hopper, it is drawn or pushed through the pipeline by the air flow generated by the pressure or vacuum system. This process ensures that the powders are transported without direct contact with mechanical components, minimizing wear and reducing the risk of contamination. The design of the conveying system is crucial, as it must accommodate the specific properties of cement and mineral powders, such as their fineness, moisture content, and flowability. Advanced models from HeadPowder incorporate optimized air flow control, ensuring consistent and efficient material transport while maintaining low energy consumption.
Key Working Scene Characteristics of the Equipment
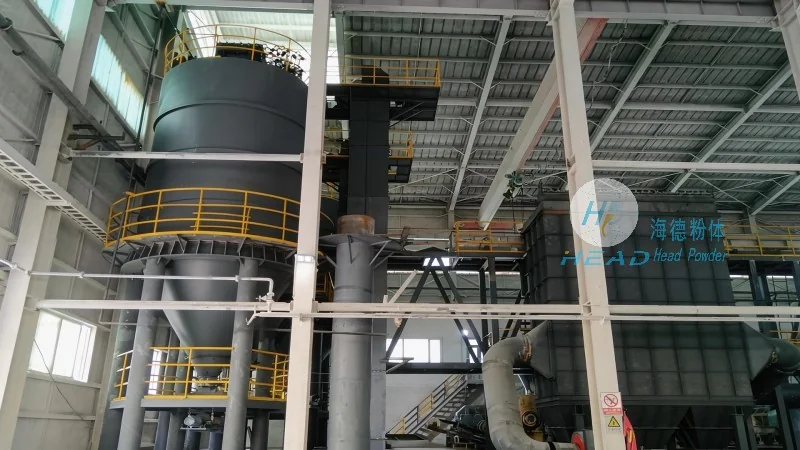
The working scene characteristics of cement and mineral powder pneumatic conveying equipment are tailored to meet the demands of diverse industrial applications. These characteristics include high efficiency in material transport, minimal space requirements, and the ability to handle large volumes of material. The equipment is particularly suitable for environments where dust control is critical, such as in cement plants, mining operations, and chemical processing facilities. Additionally, the systems are designed for easy integration into existing production lines, allowing for seamless material transfer from storage to processing units. The working scene also emphasizes safety and operational reliability, with features like automatic pressure regulation and emergency shut-off systems to prevent accidents and ensure continuous operation. HeadPowder's systems are engineered to adapt to varying operational conditions, providing consistent performance even under fluctuating material feed rates or environmental changes.
Application Scenarios and Benefits
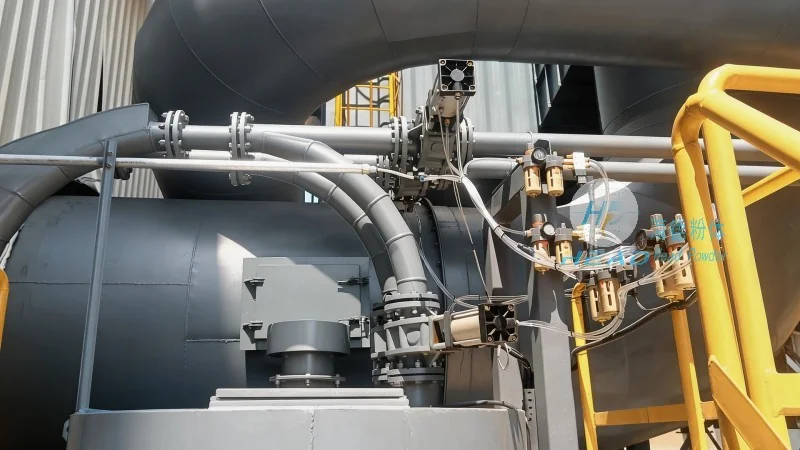
Cement and mineral powder pneumatic conveying equipment from HeadPowder is widely used in various industrial sectors. In cement manufacturing, these systems are employed to transport raw materials like limestone and clay from storage silos to grinding mills. In mining operations, they facilitate the transport of mineral powders from processing plants to storage or shipping facilities. The equipment is also utilized in chemical and pharmaceutical industries for the handling of fine powders, where precision and cleanliness are paramount. The benefits of using pneumatic conveying systems include reduced labor costs due to automated material handling, lower maintenance requirements compared to traditional mechanical conveyors, and improved product quality by minimizing material degradation and contamination. Furthermore, the systems contribute to better workplace safety by eliminating the need for manual handling of bulk powders, which can pose health risks such as respiratory issues. HeadPowder's commitment to quality and innovation ensures that their pneumatic conveying solutions meet the highest industry standards, providing reliable and efficient performance in demanding working environments.




